English
Views: 0 Author: Vinci Zhang Publish Time: 2026-10-06 Origin: Site


Nitrogen reflow soldering is a reflow process that uses nitrogen to reduce oxygen around a printed circuit board while solder paste melts. The controlled atmosphere can reduce oxidation, improve wetting, and increase process stability for demanding SMT assemblies.
Nitrogen is not a replacement for good printing, placement, profiling, or inspection. It works best when it is treated as one part of a complete manufacturing process. This guide explains how nitrogen reflow works, how to select an oxygen target, when nitrogen is useful, and how to control operating cost.
After solder paste printing and component placement, the PCB enters the reflow oven. The board passes through preheat, soak, reflow, and cooling zones. During this cycle, the paste melts and forms electrical and mechanical connections.
In a nitrogen reflow oven, nitrogen displaces much of the air inside the process tunnel. This creates a low-oxygen environment around the PCB and the molten solder.
Oxygen reacts with copper, component terminations, and solder powder at high temperature. Oxide layers can slow solder spreading and make wetting less consistent. A low-oxygen atmosphere gives the flux a cleaner environment in which to remove surface oxides.
The nitrogen reflow oven process includes gas sealing, oxygen measurement, flow control, thermal profiling, and alarm management. It is more than adding a nitrogen supply line to an ordinary oven.

Nitrogen enters through injection points or distribution manifolds. The oven design moves the gas through the heating zones while the exhaust system removes displaced air. Good equipment keeps the atmosphere stable across the board path.
Sensor location matters. A low oxygen reading at one point does not prove that every zone has the same condition. Door seals, conveyor openings, exhaust balance, and board loading can create local differences.
Production teams usually define a normal oxygen target, an alert limit, and an action limit. The correct values depend on solder paste, alloy, board finish, component density, and reliability requirements.
The target should always include a measurement location and operating condition. “Below 1,000 ppm” is incomplete if the sensor position and loading pattern are not recorded.

Nitrogen can improve solder spread on oxidized surfaces. It may reduce nonwetting, dewetting, solder balls, and inconsistent fillet appearance. The benefits are usually more visible when a product already has a narrow process window.
A useful nitrogen and air atmosphere comparison should include first-pass yield, rework cost, paste behavior, gas use, energy use, and customer requirements.
Many standard assemblies can run successfully in air. A board with generous pad geometry, stable paste, a reliable thermal profile, and adequate process margin may not gain enough from nitrogen to justify the additional cost.
Run a controlled comparison before making a decision. Keep the board revision, paste lot, stencil, profile, conveyor speed, and loading pattern consistent.
Oxide layers increase the resistance between molten solder and the pad or component termination. Solder may pull away from the surface, spread unevenly, or leave an incomplete fillet.
The purpose of oxidation control during reflow is to reduce oxygen exposure while the metal surfaces and solder are hot.
Nitrogen cannot fix a dirty PCB, insufficient paste, poor stencil release, component misplacement, or an incorrect thermal profile. Board storage, paste handling, stencil cleaning, and print inspection remain essential.
Use nitrogen to improve an identified atmosphere-related limitation. Do not use it as a substitute for basic process discipline.

Start with the solder paste supplier’s atmosphere recommendation. Then review board finish, exposed copper, component pitch, thermal mass, peak temperature, and time above liquidus.
The nitrogen reflow oxygen level should be stated with a measurement point and production loading condition.
Run a baseline at the current oxygen setting. Then test one or more lower targets using representative production boards. Inspect wetting, bridging, voiding, tombstoning, solder balls, fillet shape, and first-pass yield.
Choose the lowest target that produces a stable and economically sensible process. A lower number is not automatically better if it does not improve product quality.
Good wetting creates a continuous connection between the solder, pad, and component termination. The solder spreads over the intended pad area and forms a suitable fillet.
A controlled atmosphere can support solder wetting and joint quality by reducing the oxide burden during the liquid phase.
Use consistent inspection criteria. Combine automated optical inspection with microscope review. Use X-ray inspection for hidden joints and cross-section analysis when reliability is critical.
Track defects by type. Nitrogen may reduce nonwetting while having little effect on printing-related bridging. Separating defect causes leads to better decisions.
Nitrogen becomes more attractive when a product has fine pitch, small passive components, exposed copper, difficult surface finishes, high-temperature lead-free paste, or demanding reliability requirements.
Automotive, medical, aerospace, power electronics, and industrial assemblies may also have documented atmosphere requirements.
The nitrogen reflow application decision should include defect prevention, rework labor, scrap, field reliability, gas cost, production volume, and customer approval requirements.
A short production trial often gives more useful evidence than a general statement about nitrogen quality.
Fine-pitch pads and small terminations leave less room for process variation. A small change in paste volume, alignment, oxide condition, or thermal balance can create a visible defect.
For fine-pitch SMT assembly, nitrogen may help preserve wetting consistency. It does not replace accurate printing and placement.
Use a suitable stencil thickness, aperture design, paste type, and inspection strategy. Check component coplanarity and pad design. Profile both small and large thermal features on the same board.
Lead-free alloys generally use higher reflow temperatures than tin-lead alloys. Higher temperatures increase oxidation pressure and reduce the margin available for flux activity.
The lead-free nitrogen reflow process can support better wetting and a more stable appearance, especially when SAC alloys are used.
Lowering oxygen does not remove the need for thermal profiling. Verify ramp rate, soak behavior, peak temperature, and time above liquidus. Sensitive components must remain within their approved temperature limits.
Gas consumption depends on flow rate, operating hours, purge time, start-up cycles, standby settings, and leakage. Measure actual flow at the supply point when possible.
A practical nitrogen consumption calculation converts flow into hourly, daily, and monthly use. Add delivery charges, tank rental, and maintenance cost.
Check door seals, access panels, exhaust balance, valves, filters, and supply pressure. Use recipe-based standby settings during planned pauses.
Nitrogen flow optimization should be based on oxygen trend data and joint quality results. Reduce flow gradually and verify recovery after every change.
Evaluate temperature uniformity, zone control, nitrogen sealing, oxygen measurement, exhaust adjustment, conveyor design, maintenance access, and data logging.
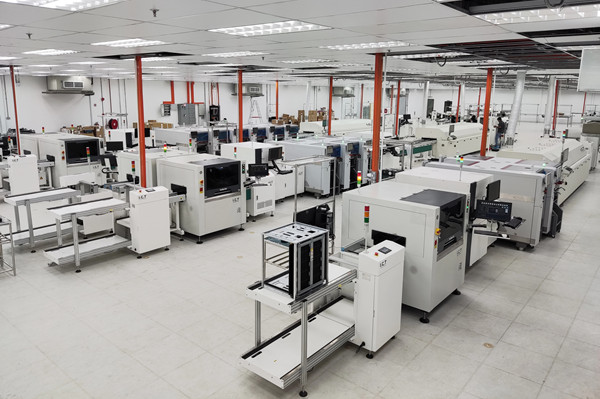
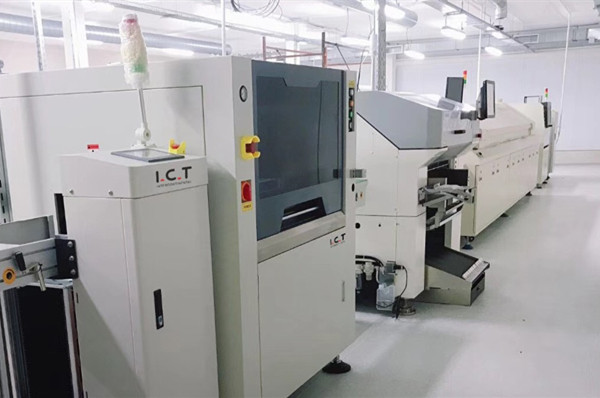
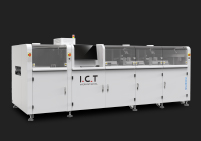
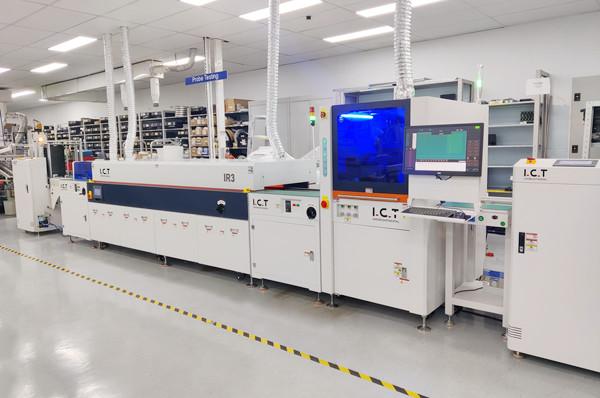
A reliable SMT reflow oven platform should maintain stable thermal performance while controlling oxygen under normal production loading.
The oven should fit the printer, placement system, inspection equipment, and traceability system. The complete SMT production line should support one consistent product recipe from printing through inspection.
A dual-rail machine can improve production flexibility, but both rails must maintain suitable thermal and atmosphere performance.
A lead-free dual-rail reflow oven should be evaluated with representative boards and normal loading conditions.
High oxygen readings may come from leaks, excessive exhaust, low nitrogen pressure, blocked filters, faulty valves, poor loading, or analyzer problems. Check mechanical causes before simply increasing gas flow.
When a line drifts, documented nitrogen reflow troubleshooting steps help operators respond consistently.
Define oxygen targets, alarm levels, measurement frequency, calibration intervals, maintenance responsibilities, and operator response steps.
Trend oxygen, flow, temperature, conveyor speed, defects, and rework together. A stable process should be reproducible across shifts, operators, paste lots, and normal production loads.
No. Nitrogen can improve oxidation control and wetting, but the improvement depends on the assembly. Air reflow may be sufficient when the board has adequate process margin. A controlled comparison is the best way to evaluate the benefit.
There is no universal oxygen value. Start with the paste supplier’s recommendation and validate it with representative boards. Define a normal target, alert limit, and action limit at a specified sensor location.
Nitrogen can reduce oxidation-related wetting problems. It cannot correct contamination, insufficient paste, poor pad design, incorrect profiling, or component coplanarity. Wetting must be evaluated together with printing, placement, and thermal data.
Check leaks, exhaust balance, valves, seals, filters, and supply pressure first. Then lower flow in small steps while monitoring oxygen recovery and joint quality. Never reduce flow only because the gas bill is high.
No. Many lead-free boards run successfully in air when the paste, finish, profile, and design are well matched. Nitrogen is more valuable when high temperature, fine pitch, difficult finishes, or reliability requirements reduce process margin.
Keep the approved profile, oxygen target, alarm limits, flow settings, analyzer calibration records, maintenance history, board loading conditions, defect data, and corrective actions. These records support process audits and make troubleshooting faster.
```