English
Views: 0 Author: Elsa Long Publish Time: 2026-11-20 Origin: Site


Every PCBA plant has quality gates. Most of them have too many, and the wrong ones. They were not chosen by anyone in particular — they accumulated, one per customer complaint, one per auditor question, one per machine that came with an inspection function because it was bundled. The result is a line where boards are examined eleven times and still escape with the defect that matters, while the one check that would have caught it was dropped years ago because it slowed the line down.
This is a PCBA factory quality gate plan written to fix that, and it takes a deliberately unfashionable position: a gate earns its place by what it can stop that the next gate cannot, not by how thorough it looks. The plan covers where gates belong from incoming material through final test, what each one owes the ones after it, and how to decide between full and sampled coverage with arithmetic instead of argument. The gate set has to be designed against a specific line, which is why every plan starts from the line configurations this gate plan has to cover rather than from a checklist of inspection methods.
The word gate implies a physical thing that opens or closes. In a factory it usually means a place where someone looks at a board and decides. Those are not the same, and the gap between them is where most quality plans fail. A gate that can only report is a checkpoint; a gate that can hold material is a control. The distinction is not semantic — it determines whether a defect found at that station stops the line or becomes a note in a spreadsheet that ships with the lot.
The practical test is short. Ask what happens to a failed board at that station. If the answer is "it goes to the rework area", that is a control. If the answer is "the operator tells the supervisor", that is a conversation. If the answer is "it gets flagged in the system", that is a record, which is valuable but is not a gate. Most plans describe a mixture of all three and call the whole thing a quality system.
This section sets out the test for keeping a gate, the two outputs each one has to produce, and where the seven gates in this plan come from. Everything after it is the application. The route that decides which gates can exist at all is settled earlier than this document — the process route that decides which gates exist at all comes first, because a plant with no coating stage has no coating gate to plan.
The difference between a checkpoint and a control is authority over material. A checkpoint observes and reports; material keeps moving while the report travels. A control can stop the board, hold the lot and refuse release until someone with authority resolves it. Both have value, but only one of them prevents escape, and escape is what quality plans exist to prevent.
Making a checkpoint into a control usually costs nothing physical. It requires three things to be written down: what condition triggers a hold, who is allowed to release it, and where the material physically goes while it is held. Plants that skip the third item discover that their hold is theoretical, because there is no defined place to put a held board and the nearest flat surface is the line itself.
The authority question is the one that gets avoided. If releasing a held lot requires a manager who is not on shift, the practical answer at three in the morning is that the hold is released by whoever is most senior on the floor, which means the gate has no authority at all. Naming two people, one per shift, with the authority to release, is a one-line policy that converts every checkpoint on the line into a control.
There is a useful consequence of taking this seriously. Once a gate can hold material, its false-positive rate becomes expensive, and the plant starts measuring it. That is healthy: a gate that flags ten boards a shift and has nine of them released without change is teaching the line to ignore it. The measurement that matters is not how many defects a gate caught, but how many holds it raised that turned out to be correct.
For every gate on the line, ask a single question: what defect class can this gate catch that the next gate cannot? If the answer is none, the gate is redundant and its cost is pure. If the answer is a class that the next gate catches later and more expensively, the gate stays. If the answer is a class nothing downstream catches at all, the gate is mandatory regardless of cost.
Applied honestly, this question removes more gates than it adds. A pre-reflow visual check that duplicates what post-reflow AOI sees is redundant unless it prevents value from being added to a bad board — which is a real argument, but a different one, and it belongs to cost rather than to detection. Two AOI stations at different points often turn out to be one station and one habit.
The question also reveals gates that exist for the wrong reason. An inspection step added after a specific customer complaint is usually placed where the complaint was found, not where the defect was made, so it duplicates a downstream gate and leaves the producing process unobserved. Moving it upstream, or replacing it with a process control on the machine that made the defect, usually costs less and catches more.
The plan below assumes a mixed-technology line: SMT, then through-hole, then cleaning and coating, then final electrical test. On that line there are seven places where a board can be stopped, and each one corresponds to a change in what the board is, not to a position on a conveyor.
Gate one is incoming: bare boards and components before anything is added. Gate two is after paste deposition, where the only thing that exists is a deposit and therefore the only thing that can be measured is a deposit. Gate three is after placement and before reflow, where components exist but joints do not. Gate four is after reflow, where joints exist and the board's electrical identity is complete for the first time. Gate five is after through-hole soldering, where a second joining process has introduced a second set of joints with different failure modes. Gate six is after cleaning and coating, where the board's surface has been changed and defects can be hidden rather than created. Gate seven is final test, where function is verified and release happens.
Seven is not a target. A single-sided board with no through-hole content and no coating has five of these gates and should not invent two more to match a template. A high-reliability board may add an eighth at X-ray review or a ninth at burn-in. The number is an output of the route and the product class, and the only rule is that each gate must own at least one defect class that no other gate owns.
Gate | Where it sits | The defect class only this gate owns | Can a downstream gate take it over |
|---|---|---|---|
Incoming | Before anything is added | Wrong part, wrong revision, mixed date code, moisture-damaged packaging | No. Nothing downstream can recover what was never verified on receipt. |
Paste | After printing, before placement | Deposit short, smeared or misregistered at a single aperture | Partly, and at the cost of a rework operation instead of a wipe. |
Placement | After placement, before reflow | Offset, missing, reversed or wrong component before value is added | Only if the post-reflow gate can attribute a cause, not just detect an effect. |
Reflow | After the oven | Hidden joint under a ball array or leadless package | No. The joint is a plane between device and pad. |
Through-hole | After wave or selective soldering | Barrel fill, hole voiding, thermal damage to a through-hole part | No. Electrical test passes a bad barrel. |
Cleanliness and coating | After wash and after coat | Ionic residue, coating pinhole, coating on a keep-out surface | No. The surface is sealed from this point on. |
Final test | After coating | Failure in the interaction between correct sub-assemblies | No. It is the only gate that exercises the board as a system. |
Each gate owes the plan two outputs, and a gate that produces only one of them is half-built. The first is a decision: pass, hold or reject, applied to a specific board or lot, by a named person. The second is a record: what was measured, against what limit, with what result, attached to an identifier that survives to the end of the line.
Most plants build the decision and defer the record. That works until the first field failure, at which point the record is reconstructed from memory and the reconstruction is always more confident than the evidence. The record is also what makes the gate improvable: a gate whose results are never collected cannot be shown to work, and a gate that cannot be shown to work is the first candidate when someone needs to save cycle time.
The two outputs have a minimum shape worth fixing once. The decision needs a limit, a result and a disposition. The record needs the same three plus an identifier and a timestamp. Five fields, and they are the same five at every gate, which is what allows a plant to join them later without a data-mapping project. A gate that invents its own record format is a gate that will be excluded from the traceability stage for reasons nobody can quite remember.
Most plants draw their process flow, put inspection symbols on it, and treat the left edge of the drawing as the start of quality control. The left edge is already too late. By the time a reel of components reaches a feeder, three things have happened that no downstream gate can undo: the material was selected, it was stored, and it was handled. Incoming control is the only place where those three are still separable, and it is the gate most often reduced to a signature on a delivery note.
The reason is not laziness. Incoming inspection sits outside the production rhythm, it has no machine to report a number, and it competes for floor space with storage. It is also the gate with the widest scope and the least tooling, which makes it feel unbounded and therefore easy to declare complete. A PCBA factory quality gate plan that starts at the line entrance has already skipped three of the decisions that determine whether the material it inspects is good. This section bounds it. It separates what incoming inspection can actually establish from what it can only pretend to establish, treats ESD as a property of a room rather than a station, and explains why a supplier certificate is evidence of a process rather than evidence of a lot. The site conditions that make any of this possible are settled before equipment arrives, which is why the readiness checks in the pre-delivery site checks that decide whether an incoming gate can work at all belong to this chapter rather than to facilities.
An incoming gate can establish identity and condition. Identity means the part in the bag is the part on the label: correct part number, correct revision, correct date code where the part is date-sensitive. Condition means the packaging and the material survived the trip: reel integrity, moisture barrier seal, humidity indicator card state, absence of visible corrosion or bent leads, solderability of a sample where the finish is suspect.
What it cannot establish is electrical performance. A plant that tests incoming components electrically is running a second test operation, not an incoming gate, and it usually discovers that the cost of that operation exceeds the value of what it finds. The exception is a specific history: a part class that has failed in the field before, at which point sampling that class is justified by evidence rather than by principle.
The distinction matters because it tells you where to put the effort. Identity and condition are cheap to check and cheap to automate with a barcode scan and a camera. Performance is expensive and rarely worth it. Plants that blur the two end up with an incoming area that scans nothing and inspects everything by eye, which is the worst of both.
There is a second thing incoming inspection cannot do, and it is the one that causes the most grief: it cannot detect a mixed lot. If a supplier ships two date codes in one bag, and both are within shelf life, and both are the correct part number, the bag passes every identity check. The failure appears later as an unexplained yield difference between two weeks of production. Counting reels against the packing list and recording the date code actually received — rather than the date code ordered — is the only defence, and it costs one field in a receiving record.
ESD control is drawn on process flows as a symbol near the line entrance, which is misleading. There is no point in the process where ESD protection happens. There is a volume of space in which it either holds or does not, and the boundary of that volume is the boundary of the gate.
There is a published floor for that volume, and it is scoped by device sensitivity rather than by factory size: the IEC 61340-5-1 withstand thresholds that set which devices an ESD programme has to cover begin at components rated 100 V human body model and 200 V charge device model. That number is worth reading twice, because it defines both who the standard covers and who it does not. A device rated below those thresholds sits outside the scope of the standard's minimum programme, which means the plant's own control has to be stricter than the standard's floor rather than merely compliant with it. Quoting compliance as an answer to a sub-threshold device is the single most common ESD argument in a factory, and it is not an argument — it is a scope statement being used as a guarantee.
So the gate has four measurable properties rather than one symbol: the resistance of the floor and the work surfaces to the common point, the integrity of the personnel grounding path including the test record for wrist straps and footwear, the charge generation of the materials in the area — including the tape, the bags and the gloves, not just the bins — and the ionisation in places where insulators cannot be eliminated. Each of those has a test and a record. A plant that can produce the four records has an ESD gate; a plant that can produce a certificate and a floor mat has a hope.
A certificate of conformance says that a supplier's process is capable of producing conforming material. It does not say that this lot was produced by that process on the day it was made, and it certainly does not say that the material in the box is the material described. Treating a CoC as a released gate is the reason incoming inspection gets audited away: the plant can show a document for every lot and a defect for every month.
The correct use of a CoC is as a substitute for measurement, not as a substitute for a gate. It allows the plant to skip dimensional verification on a part where the supplier has demonstrated capability, and it does not allow the plant to skip identity verification on that same part. Identity is cheap; capability claims are not transferable to a specific box. The gate keeps the scan and drops the caliper.
There is a hierarchy worth writing down once, because it settles most incoming arguments in a single line. A CoC replaces measurement. A first-article inspection replaces measurement for the first lot and nothing after it. A periodic audit replaces sampling frequency, never sampling existence. Nothing replaces the record that says which lot went into which build.
That last item is where incoming control connects to the rest of the plan. The receiving record is the first link in the traceability chain, and it is the only one that is created outside production pressure. If it is complete, the traceability gate in the sixth section has something to join. If it is a signature on a delivery note, the traceability gate will be built on a supplier's memory of what they shipped.
Every gate in this plan needs a place to put material it has stopped, and the incoming gate is where that requirement is most often ignored. A hold that has no location is released by default, because the alternative is a pallet in an aisle and a production supervisor asking why the line is waiting.
Three things have to exist before a hold means anything. There has to be a marked physical area, sized for a realistic hold, inside the controlled space rather than in a corridor. There has to be a status label that travels with the material and cannot be removed by the person who applied it. And there has to be a named release authority, with a deputy, whose name appears on the release rather than a department.
The sizing is worth a moment, because it is the part that gets cut in a floor plan review. A hold area sized for one pallet is a hold area that will be exceeded the first time a supplier ships a suspect lot, and the overflow will go wherever there is space, which is the line. Sizing for the largest single delivery over a month, plus the buffer that a re-inspection would need, is a planning number rather than a guess, and it costs floor area that is far cheaper than the alternative.
The other thing to fix at the same time is what happens to the material after release. A lot that was held and then released is not the same as a lot that was never held: it carries a decision, and that decision belongs in the record. A plant that records the hold but not the disposition can tell you how many lots it stopped and cannot tell you why any of them were allowed to continue, which is the question an auditor asks second and a customer asks first.

The two gates immediately after the printer are the only ones in the plan that sit on a process that has not finished yet. After paste deposition there is no joint, only a deposit. After placement there is a component sitting in that deposit and still no joint. Both gates therefore look at a promise rather than at a result, and both are judged by whether they can act on that promise before the reflow oven converts it into something expensive to undo.
This is why they are treated as a pair rather than as two independent stations. A paste gate that measures excellently but cannot communicate its verdict to the placer is a management report. A placement gate that sees a missing component but lets the board continue into reflow has converted a two-minute correction into a rework operation. The technical content of each gate is well understood; the part that fails in practice is the wire between them, and it fails for unglamorous reasons that have nothing to do with measurement capability.
The two also differ in what they can infer. Paste inspection sees the amount and shape of what was printed, which is a direct read on one process. Placement inspection sees presence, orientation and offset, which is a read on a different process and, in most plants, a read on the same defect class that paste inspection would have caught earlier if the deposit were the cause. Getting the division of labour right between the two is worth more than upgrading either.
At the paste gate the board carries information that will be destroyed by reflow. Deposit height, area, shape and the relationship between them are all measurable while the material is still soft, and all of them become unmeasurable once the material melts and wets. That is the entire justification for the gate: it is the last moment when the cause is visible rather than the effect.
What makes a paste gate useful rather than decorative is the classification of its results. Volume alone is a weak signal, because a deposit can be correct in volume and wrong in shape — a gasket of paste around an empty centre has the right volume. Area and height together distinguish a deposit that is short from one that is smeared, and those two point at different causes: a short deposit points at an aperture or a squeegee parameter, a smeared deposit points at separation speed or support. A gate that reports only volume sends the process engineer to the wrong adjustment.
The second requirement is that the gate reports per aperture rather than per board. A board-level average hides the single aperture on a fine-pitch device that is consistently a third low, and that aperture is the one that will produce the open circuit three weeks later. Per-aperture data at a board level of detail is the difference between a gate that finds trends and a gate that finds boards.
The third is the limit itself. A limit inherited from a machine default is not a process limit; it is a vendor's guess about a general case. Setting the limit from the plant's own data — printing a known-good run, measuring the spread, and setting the window at a multiple of that spread — takes an afternoon and produces a limit that means something. The machine default will still be there if the plant decides it was right.
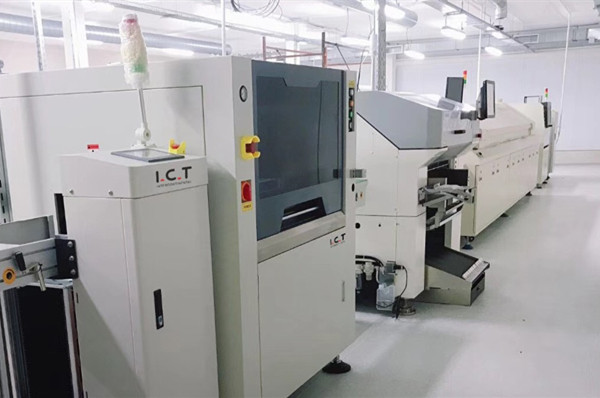
Everything above is measurement. The handshake is the part that decides whether any of it matters, and it is where a real project in this industry spends its time. According to I.C.T project records, an SMT plant that replaced its paste inspection station spent 4 days on site, and the work was not primarily about inspection capability. The four problems that consumed those days were all interface problems: the inspection system and its server computer could not talk to each other at the start; a machine had its hostname bound to an old IP address and refused to accept the new one; the fail signal output by the inspection system did not match the pin the receiving equipment expected; and the inspection server software could not reach its database.
Read that list again, because it is a complete taxonomy of why gates fail in the field. Two items are network identity, one is signal convention, one is a service dependency. None of them is a measurement problem, and all of them can leave a plant with a fully capable inspection station that has no effect on what reaches the oven. A plant buying a gate should budget engineering time for the interface, not just for the machine.
The design rule that follows is simple and unpopular: the handshake must be tested with a deliberately bad board before the line runs production. Not a simulated fail signal in software, and not a demonstration by the vendor — a real board with a real defect, placed in the line, with the placer in automatic mode, and a stopwatch on how long it takes the line to halt and where the board physically ends up. If the board continues into reflow, the gate does not exist regardless of what the report says.
There is a second half to the handshake that gets even less attention: what happens after the stop. A halted line with a board in an undefined position is a recovery problem, and the recovery procedure is part of the gate. Where the board is removed, who authorises the re-inspection, and whether the placer resumes from the same board or from the next one are all decisions that should be written before the first stop rather than improvised during it.
Placement verification asks a narrower question than paste inspection: is the right component in the right place, in the right orientation, and is anything missing. On a line that already has a paste gate and a post-reflow optical gate, the marginal value of a dedicated placement inspection station is often low, because most placement errors that matter also produce a paste anomaly or a post-reflow signature.
That does not mean the gate is absent; it means the gate can be carried by the placer itself. Modern placement machines verify pickup, check nozzle vacuum, measure component presence before placement, and can re-pick a component that failed the check. That is a control in the sense this plan uses the word: it acts on material before value is added, and it does so without a separate station. The plant's obligation is to make those machine-level checks visible in the record rather than leaving them as internal counters nobody reads.
On STB panels the placement gate has to be judged per panel rather than per board, because a panel-level offset produces a characteristic pattern — good boards on one side, drifting boards on the other — that a per-board statistic averages away. This is the reason panel-level lines are planned differently from single-board lines, and it is visible in how STB panels, where the placement gate is judged per panel instead of per board are set up: the gate's unit of judgement follows the unit of assembly.
Where a dedicated placement gate does earn its place is the case where the cost of continuing is high and the paste gate cannot see the cause. A board with a large, expensive device placed at an angle will pass a paste check and fail at reflow in a way that damages both the device and the board. That is a specific, expensive, downstream-invisible defect class, which is exactly the test this plan uses for keeping a gate.
On a mature line with good printing control, paste inspection and placement verification frequently collapse into a single combined station, or into a paste gate plus machine-level placement verification with no station at all. That is a legitimate outcome of the redundancy question, not a compromise. It is legitimate when three conditions hold: the paste gate reports per aperture, the placer's own checks are recorded, and the post-reflow gate can distinguish a placement defect from a soldering defect.
The third condition is the one that is usually assumed rather than verified. If the post-reflow optical gate cannot tell a tombstoned component caused by a poor deposit from one caused by a placement offset, then collapsing the earlier gates removes the plant's ability to route the defect to the right process. The gates were not redundant; they were the only source of attribution.
The practical test is a small experiment rather than a policy debate. Deliberately induce three failures — a short deposit, an offset placement, a missing component — and run the boards through the collapsed gate set. If each failure is routed to the correct process, the collapse is safe. If two of them produce the same report, the collapse has removed a gate that was doing diagnostic work under a different name.
Where the collapse is safe, it is also cheaper in a way that is easy to underestimate. Every station removed is a station that no longer needs a handshake, a recovery procedure, a limit review and an operator qualification. On a line that will run for years, the maintenance of a gate costs more than its purchase, and a fully automatic STB line, where the placement gate has to run without anyone watching it shows the trade clearly: the fewer stations that need attention, the more of the line's uptime survives a shift change.
Gate four is the first gate in the plan that looks at a finished thing. Up to now every measurement has been a measurement of intent: a deposit that should become a joint, a component that should be joined. After reflow the board has joints, and for the first time its electrical identity is complete — every connection that will ever exist on the top side now exists, including the ones that should not.
That completeness is what makes the gate both powerful and expensive. It is powerful because a joint is the thing the customer will test. It is expensive because a joint has more ways to be wrong than a deposit does, and several of them are underneath a component where no camera can reach. The entire design problem of gate four in any PCBA factory quality gate plan is the allocation between what can be seen from above and what cannot, and the mistake most plans make is to treat that as a binary choice between optical inspection and X-ray rather than as a budget to be graded.
There is also a timing property that distinguishes this gate from all the others. It sits after the point of no return for the SMT side: a board that passes gate four badly cannot be fixed by adjusting the printer, because the evidence that would have pointed at the printer has melted. Whatever gate four cannot attribute, gate two has already lost the chance to explain. That is not an argument for moving gate four earlier — it cannot be moved — but it is an argument for keeping gate two's records joined to gate four's, so that attribution survives the oven.
An optical gate after reflow sees the surface of the board: fillet shape, wetting angle, component presence, polarity marks, solder balling, tombstoning, bridging on visible leads, and the general topography of the joint. Those are direct observations and they are reliable when the joint is exposed.
What it infers is everything underneath. A ball grid array joint, a bottom-termination component, a leadless package — the joint that matters is a plane between the device and the pad, and no camera above the board will ever see it. The gate can report on the device's alignment and on the solder that squeezed out at the edge, and both of those correlate with the hidden joint without being the hidden joint. Correlation is useful and it is not detection, and the plan should say which one the gate is doing.
The distinction has a practical consequence for how limits are set. A limit on visible fillet height is a limit on a real measurement. A limit on the amount of visible solder at a package edge, used as a proxy for hidden joint quality, is a limit on a correlation — and correlations drift when the supplier changes the package or the stencil changes the aperture. Limits of the first kind can be set once and reviewed annually. Limits of the second kind need re-establishing whenever the input changes, and a plant that does not know which kind it has will keep a proxy limit for years after it stopped meaning anything.
There is one product class where the optical read is the primary read rather than a proxy, and it is worth naming because it changes the gate's design. On LED assemblies the failure that matters is often optical before it is electrical: a joint that is electrically continuous but has poor thermal or optical contact shows up as a colour or brightness difference, not as an open. That means LED boards, where the post-reflow gate has to be read as an optical measurement first need a gate that can compare a device against its neighbours on the same board, which is a different capability from detecting a defect against an absolute standard.
The honest statement of the optical gate's limit is that it cannot distinguish three cases: a joint that is good, a joint that is bad but hidden, and a joint that is marginal and will fail in the field after thermal cycling. All three look identical from above. The gate's report on a hidden joint is therefore not a measurement but a probability, and the plant's release decision is being made on that probability whether or not anyone says so out loud.
This is not a reason to distrust optical inspection. For the majority of joints on a typical board the joint is exposed, and the optical gate measures it well. The problem is the minority: the devices that carry the highest value, the highest pin count and the highest consequence of failure are disproportionately the ones with hidden joints. A gate that is strong where the risk is low and blind where the risk is high is not a bad gate, but it is a gate whose coverage has to be completed rather than assumed.
The completion is X-ray, and the question is never whether to have it. The question is how much of the board, how often, and at what point in the flow. Those three answers are where plans diverge, and where the arithmetic in the final section becomes the deciding argument rather than a tiebreaker.
The usual debate poses X-ray as all or nothing: either every board goes through the machine or the machine is a sample-check tool for engineering. Both positions are defensible and both are usually wrong, because they treat coverage as a single number when it is at least three.
The first dimension is spatial: which joints are in scope. X-raying every joint on every board is rarely justified; X-raying the joints under the largest and finest-pitch devices on every board frequently is. Defining the scope by device class rather than by board means the coverage survives a board revision, which a board-level rule does not.
The second dimension is frequency: every board, every panel, every lot, or every shift. The right frequency follows the stability of the process that produces the joint. A process that has been stable for a year and is monitored by upstream gates does not need per-board confirmation; a process that just changed its paste, its profile or its supplier does. Tying frequency to change events rather than to a calendar is what makes the coverage respond to risk.
The third dimension is the disposition rule: what happens when the X-ray finds something. A finding that triggers a hold on the board is a control. A finding that generates an image stored for later is a record. A finding that triggers a hold on the lot, plus a review of every board produced since the last good check, is what a well-designed gate does — and that third rule is the one that converts a sampling tool into a gate with real authority.
Coverage dimension | The question it answers | A rule that survives a board revision |
|---|---|---|
Spatial | Which joints are in scope | Defined by device class — ball array, leadless, fine pitch — rather than by a list of reference designators, which change with every layout. |
Frequency | How often the scope is examined | Tied to change events: new paste, new profile, new supplier, new stencil. A calendar-based frequency stays the same while the process moves. |
Disposition | What a finding does to material | Hold the lot, then review every board produced since the last accepted check. Holding one board is inspection; holding the interval is control. |
Record | What survives to the investigation | Image, limit, result and identifier, retrievable by device class rather than by date. Date-based retrieval answers the wrong question. |
Every inspection station produces boards it cannot classify. The image is ambiguous, the operator is uncertain, the limit sits exactly at the measured value. What happens to those boards is a better indicator of a plant's quality system than its first-pass yield, because it is the moment when the system has to decide without evidence.
Three dispositions are possible and only one of them is a gate. The board can be passed, which resolves the ambiguity in favour of production and teaches the operator that uncertainty is harmless. The board can be scrapped, which is safe and expensive and will be quietly avoided. Or the board can go to a defined arbitration step — a second reviewer with different information, a cross-section, a functional test at that specific net — with a named owner and a time limit.
The arbitration step is what makes the gate improvable, because the cases that reach it are exactly the cases where the gate's limits are wrong. A plant that logs arbitration outcomes and reviews them monthly is running a self-correcting gate. A plant that logs only pass and fail is running a gate whose blind spot is permanent and invisible.
The time limit matters as much as the owner. An arbitration that takes three days is an arbitration that production will route around by finding a way to pass the board. An arbitration that resolves within the shift, even if the resolution is "hold the lot and investigate tomorrow", keeps the gate inside the production rhythm where it can actually function.

The two gates after reflow share a property that none of the earlier ones have: both are inspecting a board whose electrical function is already complete. A through-hole defect does not change what the board computes, and a coating defect does not change it either, at least not on the day it is made. Their consequences are delayed, which is exactly why they get less attention than the gates that produce a number on the first pass.
That delay is the reason these gates need a different design logic. An electrical fault announces itself at final test; a joint that will crack after a thousand thermal cycles, or a coating that traps a residue under it, does not. The only way to control a delayed failure is to control the process that produces it and to measure the property that predicts it, which means these two gates are as much about process evidence as about board inspection.
There is also a sequencing constraint that is easy to get wrong when you lay out a PCBA factory quality gate plan. Cleanliness comes before coating, and coating hides everything that comes before it. A plant that inspects coating thoroughly and cleanliness casually has put its most capable gate after its least capable one, and the good gate will be reporting on a surface that was already contaminated when it was applied.
Through-hole soldering introduces a set of joints that fail differently from SMT joints. A reflow joint fails at the interface between the deposit and the pad. A through-hole joint fails through the barrel: insufficient fill, voids in the barrel, a fillet that wets the pad but not the lead, or thermal damage to a component that was never designed to see a wave.
Those failure modes are not visible from the same angle as SMT defects. Barrel fill is inside a hole; a fillet that looks correct from above can be a cold joint underneath; and the thermal damage caused by preheat that was set for the mass of the assembly rather than for the sensitivity of one part shows up as a component that works today and drifts next month. The inspection at this gate has to be specified in terms of those failure modes rather than in terms of "visual inspection", which is a description of the method and not of the question.
What the gate can establish directly is fill and wetting on visible joints, component seating, polarity, and the absence of bridging between adjacent pins. What it establishes statistically is barrel fill on the joints it can see from the side, which is a sample of a population whose worst members are usually the ones in the middle of a connector body. The gap between those two is where selective soldering earns its cost, because a process that controls the volume delivered per hole is a process control that substitutes for an inspection that cannot reach.
The other thing this gate owes the plan is a process record rather than a board record: preheat profile, flux type and amount, wave or nozzle parameters, and the identity of the operator. A through-hole defect found at final test is almost never diagnosable from the board, and is usually diagnosable from the process record within a few minutes. That record is the second output this plan requires of every gate, applied to a gate where it matters more than the first.
Cleaning is a process, cleanliness is a property, and a gate has to measure the property. The confusion between the two is the reason plants can describe their wash cycle in detail and cannot state how clean their boards are. Running the machine is evidence that the process happened; it is not evidence of the result.
What makes this gate awkward is that the property is not visible. Residue that matters is often ionic and colourless, and the flux that remains after a no-clean process is a deliberate engineering choice rather than a defect — until the coating goes on top of it. The gate therefore has to be specified against the process the board will actually receive: a board going into a coating has a different cleanliness requirement from a board going into a sealed enclosure with no coating, and applying the stricter requirement to both is a cost that buys nothing.
The measurement itself is a sampling operation with a defined extraction method, and the number it produces is only comparable to other numbers produced the same way. Two plants can both report a conductivity reading and be measuring different things if their extraction differed. That is worth stating explicitly in the control plan, because the most common failure of a cleanliness gate is not a bad result — it is a result that cannot be compared to the last one.
The environment around the gate is a separate variable, and it is the one with a published classification. Air cleanliness in a controlled zone is graded by particle concentration under the ISO 14644-1 classification that grades air cleanliness by particle concentration, and a coating area that is graded while its incoming air is not filtered to match is a graded room with an ungraded supply. The classification is a property of the zone, and it holds only while everything crossing its boundary is controlled.
Coating is the only process in the plan that can convert a passing board into a failing one without adding or removing anything electrical. A coating applied over a contaminated surface traps the contamination and moves its failure from "cleanable" to "sealed in". A coating with a pinhole at a via creates a corrosion path that did not exist before. A coating applied too thickly at a connector causes a mechanical failure at mating.
That is why the coating gate has to inspect three things and not one. The first is coverage: whether the intended area is coated. The second is integrity: whether the coating is continuous, which is a different question from coverage and requires a different method — visual inspection under ultraviolet, or a test coupon processed alongside. The third, and the one most often skipped, is the absence of coating where it must not be: connector contacts, test points, keep-out zones and any surface that has to remain solderable.
The third item is where coating gates fail in a way that reaches customers. A connector with coating on its contacts passes a coverage check, passes an integrity check, and fails at the customer's mating operation weeks later. Verifying the keep-out zones is cheap, visual and boring, and it is the check that a gate under time pressure drops first because the board looks fine.
On products where the enclosure seals the board for its whole service life, this gate carries more weight than final test does, because nothing downstream will ever look at the board again. That is the situation on drone control boards, where cleaning and coating gates sit ahead of final test because the enclosure is closed for the life of the unit — and where a coating defect is not a rework cost but a field return with no diagnosis path.
Cleanliness and coating are usually managed by two different groups with two different records, and the join between them is where the plan's second output requirement pays off. The cleanliness result has to travel with the lot into the coating gate, because the coating gate's disposition depends on it: a lot with a marginal cleanliness result should not be coated without a decision, and a lot that was cleaned twice should be coated with that history attached.
In practice this means the coating gate reads two inputs and writes one decision. The inputs are the cleanliness result and the visual condition of the board at coating entry. The decision is coat, hold, or reclean. A plant that records the decision but not the two inputs has a gate that cannot answer the only question anyone will ask after a field failure: was this board coated over a known marginal surface.
The join also settles an argument that recurs whenever coating defects appear. If the cleanliness record is complete, the argument about whether the defect came from the wash or the coating is answered by data in minutes. If it is not, the argument is settled by seniority, and the process that gets changed is whichever one has the quieter representative.
Every gate so far has a position on the conveyor. Traceability has none. It is drawn on process flows as a box somewhere near the end, which is misleading in the same way that an ESD symbol near the line entrance is misleading: the thing being described is a property of the whole flow rather than a place in it.
A traceability gate is a rule about what has to be recorded at every other gate, plus a join that makes those records retrievable as one story. It is a gate in the sense this plan uses the word because it can hold material: a lot whose records are incomplete can be refused release. It runs sideways because its input is every station's output and its verdict applies to the lot rather than to the board in front of it.
That sideways position is why traceability is the last thing most plants build properly and the first thing customers ask about. It produces no yield improvement, it does not reduce defects, and its entire value is realised on the worst day in the plant's year — when a customer reports a failure and the plant has to say what else was built the same way. A gate whose only payoff is on that day is a gate that gets deferred, and deferring it is a decision that is only visible in hindsight.
The technical core of traceability is a single identifier that every gate writes and every query can read. In most plants this is a serial number or a panel code applied at the first station, and the choice of how it is applied — laser mark, label, printed code, etched — determines what the rest of the system can do.
The constraint that decides it is not cost. It is whether the identifier survives every process the board goes through. A label that survives printing and reflow may not survive cleaning, and a code that survives cleaning may be unreadable after coating. Discovering this after the coating line is installed means either adding a re-marking station, which is a new gate nobody planned, or accepting that traceability stops before coating, which is usually the process the customer most wants traced.
The second constraint is the reader, and it follows from the first. A code that is readable by a camera at one station and not at the next forces the plant to standardise on the weaker reader, which usually means buying better readers than the application strictly needed. That is cheaper than the alternative, which is a mixed population of readers and a rule that some stations record manually.
Manual recording is the failure mode to design out at this stage. A station that records by hand does so accurately for the first month, approximately for the second, and not at all once the line runs at rate. The identifier decision is therefore a decision about which stations can be automated, made before the automation exists.
Traceability is usually specified as a level rather than as a boolean, and the published framework for that is IPC-1782, where minimum requirements rest on four levels of traceability for materials and processes. The important part of that definition is the word minimum: the levels describe what has to be recorded, and the choice among them is supposed to follow the risk of the product rather than the ambition of the quality manager.
Read as a cost curve, the levels behave the way most quality investments behave. The first level — knowing what went into a lot — is cheap, because the information already exists in the receiving record and the material issue record. The middle levels add process parameters and machine identity, which means instrumenting stations that currently have no reason to export data. The highest level adds per-unit history, which means a unique identifier on every board and a data store that can answer a query about one unit years later.
The mistake is to select the highest level for every product because a customer once asked. The cost of the highest level is not the identifier; it is the discipline of recording at every station, forever, including on the shifts where nothing is being audited. A plant that chooses a level it cannot sustain ends up with records that are complete on paper and unreliable in fact, which is worse than a lower level honestly applied — because the lower level's gaps are known and the higher level's are assumed away.
The defensible rule is to set the level per product family by consequence: what the plant would have to do if a single unit failed in the field. If the answer is "replace it and move on", a low level is proportionate. If the answer is "recall a lot and prove what else is affected", the level has to be high enough to answer that question without reconstruction. The level follows that answer, not the other way round.
The equipment cost of traceability is visible and gets budgeted. The record cost is invisible and does not, which is why traceability projects are usually late by the amount of work nobody counted.
At the material level the record cost is one scan per reel issue, which is a few seconds and a training requirement. At the process level it is an export from each machine, which means a protocol, a parser, and someone who owns the parser when the machine firmware updates. At the unit level it is a write at every station plus a query interface, and the query interface is where the real cost sits: a data store that can hold the records is cheap, and one that can answer "show me every board that shared this reel" in under a minute is a design problem.
There is a fourth cost that sits outside the levels and is usually discovered last: the cost of the record being wrong. A traceability system that reports a reel as having been used on a lot it never touched is worse than no system, because it directs an investigation at the wrong product. Validating that the join is correct — by deliberately scanning a wrong reel and confirming the system rejects it — is a test that belongs in the acceptance criteria and rarely appears there.
This is the same sequencing argument that applies to the plant itself, which is why building the plant in stages that put traceability after the process gates are stable is the cheaper order. A traceability system built on top of processes that are still changing records a moving target, and every process change becomes a data-model change.
For traceability to be a gate rather than a report, it needs the authority to stop a lot. That authority is exercised at the point of release, and it is a checklist rather than a judgement: every gate that should have written a record has written one, the join key resolves, and no lot in the build has an open hold.
Two design details make that checklist work. The first is that the check is automatic and blocks release, rather than being a report someone reviews. The second is that it names what is missing specifically enough to be fixed — "station four has no record for panels after the midday break" is actionable in a way that "traceability incomplete" is not.
The refusal itself needs the same treatment as any other hold: a defined location for the material, a named release authority, and a disposition that gets recorded. A traceability hold that is released by overriding the system teaches the plant that the gate is advisory, and once that lesson is learned it is not unlearned by adding fields to the checklist.
What makes this gate worth its cost is not compliance. It is that a complete record makes every other gate improvable, because it allows a field failure to be traced back to the station that produced it. A plant with traceability can ask which gate should have caught a defect. A plant without it can only ask who was on shift.
Final test is the gate everyone trusts and the only one that proves the least. It verifies that the assembly functions at the moment it is tested, in the conditions of the test, with the test program that was written for it. Everything outside that envelope — thermal margin, long-term drift, a joint that is mechanically sound today and cracked in a year — is invisible to it. That is not a criticism; it is a definition of scope, and the scope is narrower than most release decisions assume.
What final test does uniquely well is the one thing no earlier gate can do: it exercises the board as a system. A correct deposit, a correct placement and a correct joint can still produce a board that does not work, because the failure is in the interaction rather than in any single operation. Only a functional test sees that, and it is the reason the gate stays regardless of how good the earlier gates become.
The economics of a PCBA factory quality gate plan converge here, because final test is where coverage decisions get expensive and where the arithmetic is easiest to make explicit. The rest of this section does that arithmetic with deliberately round numbers so the method is visible and the conclusion is not confused with a claim about any particular plant.
A functional test proves the assembly works within its test conditions. The three failure classes it cannot see are worth naming, because each one belongs to a different gate upstream.
The first is the marginal joint: continuous at room temperature, open after thermal cycling. It passes final test and fails in the field, and the only gate that can address it is the joint gate — either through coverage or through process control. The second is the latent component: a device damaged by ESD or by thermal exposure that still functions but has reduced margin. That failure belongs to the ESD gate and the through-hole gate's preheat record. The third is the sealed-in residue: contamination under a coating that will corrode slowly. That belongs to the cleanliness gate, and it is the reason a coating applied over an unmeasured surface is a decision rather than a process step.
The practical consequence is that final test cannot be improved to compensate for weak upstream gates, and plants that try end up adding test coverage for failures that a cheaper gate would have prevented. A test that takes another minute per board to catch a marginal joint is a test that costs more per year than the inspection station that would have caught the cause.
What final test should carry beyond pass and fail is the failure signature: which test failed, on which net, in what pattern across the lot. A lot where the same net fails on consecutive boards is a process problem that has already been diagnosed. A lot where failures are scattered is an assembly problem. That distinction is only available if the test results are recorded per board rather than counted.
The following figures are assumed values chosen for arithmetic, not measurements from any customer project. They are round on purpose, because the method is the point.
Assume a line with seven gates, a monthly volume of 5,000 boards, an optical inspection gate costing USD 0.35 per board in depreciation and labour, and a cost of USD 120 to resolve one board that escapes to a customer — covering rework, freight and the handling of the complaint. Assume further that without the gate, 2% of boards would carry the defect the gate is designed to catch.
Full coverage costs 5,000 × USD 0.35 = USD 1,750 per month. Not having the gate costs 5,000 × 2% × USD 120 = USD 12,000 per month. The gate pays for itself at a defect rate far below the assumed one: the crossover sits at USD 0.35 ÷ USD 120 = 0.29%. Any defect class occurring more often than that justifies full optical coverage on cost alone, before any argument about customer confidence.
Now run the same arithmetic on a gate that is an order of magnitude more expensive per board. Assume an X-ray gate at USD 8 per board, and the same USD 120 escape cost. The crossover is USD 8 ÷ USD 120 = 6.7%. A hidden joint defect that occurs at around 0.5% of boards is well below that line, which means full X-ray coverage does not pay back on escape cost alone at that frequency. The conclusion is not that X-ray is unnecessary; it is that X-ray has to be justified by consequence rather than by frequency — a high-reliability product where one escape costs far more than USD 120 changes the answer, and so does a defect class where the escape cost includes a recall.
Two limits on the method are worth stating. The first is that escape cost is usually underestimated, because it excludes the engineering time spent on the investigation. The second is that the two gates are not independent: adding the optical gate reduces the defect population that reaches the X-ray gate, which raises the X-ray crossover. The arithmetic should therefore be run in the order the gates appear on the line, not in isolation.
Gate type | Assumed cost per board | Assumed escape cost | Crossover defect rate | What the arithmetic concludes |
|---|---|---|---|---|
Optical, after paste or after reflow | USD 0.35 | USD 120 | 0.29% | Full coverage pays back on escape cost alone at almost any realistic defect rate. At 5,000 boards a month the gate costs 1,750 and the escapes it prevents cost 12,000 at a 2% rate. |
X-ray on hidden joints | USD 8 | USD 120 | 6.7% | Full coverage does not pay back at a 0.5% defect rate. Grade the coverage by device class and justify the gate by consequence rather than by frequency. |
Every figure in that table is an assumed value chosen to make the method visible, not a measurement from any project. Substituting your own escape cost is the only step that changes the conclusion, and it is the step most plants skip.
Run honestly, the arithmetic almost never produces "all gates at full coverage". It produces a graded plan, and the grades follow the shape of the cost curve rather than a policy.
Cheap gates with broad defect coverage — optical inspection after paste and after reflow, and the identity checks at incoming — justify full coverage on cost alone. Their crossover rates are low enough that nearly any real defect rate clears it.
Expensive gates justify coverage concentrated where consequence is highest: every board for the joints under the largest and finest devices, sampled for the remainder, with frequency tied to process change events rather than to a calendar. That is not a compromise between full and sample; it is a different variable being optimised, and it is the correct answer to a question that the all-or-nothing framing never asked.
The third grade is the gate that cannot be justified at all on cost and is kept anyway, on consequence. A functional test on a safety-related assembly is the standard example. Keeping it should be a recorded decision with a named owner, not a default, because a gate kept without a stated reason is the first gate cut when the reason is forgotten.
What makes the graded plan work in practice is that each grade carries a different review rhythm. Full-coverage gates get their limits reviewed when the process changes. Sampled gates get their frequency reviewed when the escape history changes. Consequence-justified gates get reviewed when the product's risk classification changes. Three rhythms instead of one annual audit is more work and catches more.
The last design question is authority, and it is the one that turns a written plan into a system that operates at three in the morning. Every gate in this plan produces a disposition, and every disposition has a signer. If the signer is a role rather than a person, the role will be filled by whoever is present, and the gate's authority will be whatever that person is willing to spend.
The workable structure names two people per gate, one per shift, with a named deputy for absence. It also separates two authorities that are usually merged: the authority to release a held board, and the authority to change a limit. Merging them means the person under pressure to ship is also the person who can redefine what passing means, and the second authority will eventually be used to resolve the first.
Where the signer sits outside the plant, the arrangement has to be written before the first hold rather than negotiated during it. A gate whose release requires a customer's quality engineer will sit idle over a weekend, and the material will move anyway under a verbal approval that nobody records. the responsibility matrix that assigns sign-off between supplier, customer and contractor is where that arrangement belongs, and it is worth settling at the same time as the gate list rather than after the first dispute.
Planning a gate set for a line that does not exist yet
Most of the cost of a quality gate plan is decided before the equipment order, because the gates that can exist are limited by the line that is bought: a printer without closed-loop paste control cannot feed a paste gate, a line without a network cannot support a handshake, and a board without a durable identifier cannot be traced past cleaning. The reverse is also true, and it is the expensive direction. A gate set specified after the order is a gate set fitted around equipment chosen for other reasons, and every compromise is then made by the process engineer in the first month of production rather than by the buyer at the specification stage. If you are specifying a line and want the gate plan and the line configuration designed together, send the board mix and the defect history you already have. We will come back with the gate positions, the coverage grades and the interface points that have to be written into the purchase specification.
There is no correct number, and any plan that quotes one is describing a template rather than a line. The workable rule is that each gate must own at least one defect class that no other gate owns. A single-sided board with no through-hole content and no coating typically ends up with five gates; a mixed-technology board with coating and traceability requirements ends up with seven or eight. The count is an output of the route and the product class, so two plants running similar equipment can legitimately have different gate counts.
Usually yes for SPI, and conditionally for AOI. Paste inspection sits at the only point where the deposit is still measurable and the cause of a defect is still visible, which makes it hard to replace. Post-reflow optical inspection carries a different question — whether a joint was formed — and its marginal value depends on whether the earlier gates and the placer's own checks already cover the placement defect classes. The test is whether the post-reflow gate can distinguish a placement defect from a soldering defect. If it cannot, removing the earlier gates removes the plant's ability to attribute, not just its ability to detect.
On cost alone, rarely. With an assumed X-ray cost of USD 8 per board and an assumed escape cost of USD 120, full coverage only pays back when the defect it catches occurs at roughly 6.7% or more. Most hidden-joint defects occur far below that, which is why the workable answer is graded coverage: every board for the joints under the largest and finest-pitch devices, sampled elsewhere, with frequency tied to process changes. The exception is consequence. A product where one escape triggers a recall changes the escape cost by an order of magnitude and can justify full coverage on its own.
Both, and they answer different questions. Coating inspection is the last gate that can see the surface before it is sealed, so it belongs immediately after coating and before any handling that could damage the coating. Functional test belongs after coating because the coating process itself can cause failures — a coated connector, a coating bridging a test point — and testing before coating would miss them. The order that works is coat, inspect the coat, then test, with the test result recorded against the same identifier the coating gate used.
Often yes, provided the machine's checks are recorded rather than left as internal counters. Modern placers verify pickup, monitor nozzle vacuum and confirm component presence before placement, which is a genuine control because it acts before value is added. What they do not do is produce a retrievable record per board unless the plant configures it to, and a check that leaves no record cannot support attribution later. The condition for dropping the station is that the post-reflow gate can still tell a placement defect from a soldering defect; if it cannot, the station was doing diagnostic work under an inspection name.
Three things. It has to be able to refuse release, which means the completeness check blocks the release step rather than generating a report. The join key has to survive every process the board goes through, including cleaning and coating, which is a decision made when the marking method is chosen and not afterwards. And the level has to match the consequence of a field failure, because a level the plant cannot sustain produces records that are complete on paper and unreliable in fact — worse than a lower level honestly applied, since the gaps are hidden rather than known.
Introduce a deliberate failure and watch what the system does with it. A board with a real defect, placed in the line in automatic mode, with a stopwatch on how long the line takes to halt and where the board physically ends up. Do that for each gate in the plan, and also for the handshake between gates, because the interface is where most gates fail in practice — network identity, signal convention and service dependencies account for more lost gate function than measurement capability does. A gate that passes the induced-failure test is a gate; one that only passes a document review is a station with a procedure attached.