English
Views: 0 Author: Elsa Long Publish Time: 2026-11-20 Origin: Site


Most factories are not built in one decision. They are built in three or four, spread over two or three budget cycles, and the first decision quietly determines how expensive the rest become. A plant that starts with SMT and later adds through-hole, coating and traceability does not fail because the later stages were wrong. It fails because the first stage left no room, no capacity and no data path for them, so every addition becomes a demolition job performed around a running line.
This is a phased PCBA factory expansion plan written from that angle. It does not re-run the question of which process route to choose — that belongs to the route decision that has to be settled before the first phase is scoped. It answers the next question: given the route, in what order do you build it, what does each stage have to leave behind for the next one, and how do you know when a stage is finished. The equipment each phase grows out of is described under the line configurations that each build phase has to grow out of, because a phase plan is only ever a plan for a specific line, not for a machine category.
In construction a phase is a contract milestone. In a PCBA plant it is a capability that has been proven and can now be used as a foundation, which is a much stricter definition. The difference matters because a plant that treats phases as milestones ends up with four partially finished capabilities and no stable one, while a plant that treats them as proof points can stop after any stage and still be a working factory. Everything that follows depends on which of those two readings the project adopts at the outset.
There is also a physical constraint that no budget schedule can argue with. Each stage adds a class of process the previous stage did not have: surface mount adds a thermal process, through-hole adds a second joining process with its own exhaust and fixtures, coating adds a wet chemistry room with a cure step, and traceability adds a data layer that has to attach to every one of them. You cannot install the data layer before there are processes producing the data, and you cannot install the chemistry room after the floor plate has been committed to conveyors. The order is not a preference. It is the only order in which each stage has something to attach to.
Ask a plant engineer why SMT comes first and the honest answer is usually about capital, but the technically correct answer is about what each stage needs from the shell. SMT needs a clean floor, a level slab, a conveyor corridor and stable power. THT needs all of that plus extraction at the soldering station and a fixture store. Coating needs all of that plus a separate room with controlled access, a chemical store, an exhaust system sized for solvent load and a make-up air path that does not disturb the pressure balance of the SMT hall. Traceability needs almost nothing physical — a few network drops and a place to put a marking station — which is exactly why it is always deferred and always the most disruptive when it finally arrives, because by then every process has been designed without a place to read an identifier.
The budget logic and the building logic point the same way, but for different reasons. A plant that builds SMT first can start earning before it commits to a coating room, and it can decide the coating question using measured data — how much of the product mix actually needs protection — rather than a forecast. The building logic says the same thing from the other side: the floor, the power and the exhaust header are cheapest before the first conveyor is anchored, so the parts of later stages that belong to the shell should be paid for in stage one even though their equipment is bought in stage three. Separating those two purchases is the whole discipline of phasing. Equipment follows demand; interfaces follow the building.
Defining stages by equipment list is the most common planning mistake, because equipment lists change and capabilities do not. Defined by capability, the five stages are stable and each one has an unambiguous exit condition.
Stage one is a working SMT process: printing, placement, reflow and at least one inspection point that closes the loop, producing boards that a customer will accept. Stage two adds a second joining process for through-hole content, which means insertion, a soldering method, post-solder inspection and the fixtures that make insertion repeatable. Stage three adds protection: cleaning where flux residue matters, and conformal coating where the service environment demands it, together with the room, the cure path and the masking labour that come with it. Stage four adds identity: every board or every lot carries a record that can be retrieved later, produced by the processes that already exist rather than typed in afterwards. Stage five adds the layer that connects them — an execution system, material control at the point of use, and automation where a measured bottleneck justifies it.
Written this way, each stage has a property the equipment list cannot give you: you can tell whether it is finished. A stage that is "the second placement machine" is never finished, because there is always another machine. A stage that is "a through-hole process with a fixture and a post-solder inspection step" is finished on a specific day, and that day is when the next stage's clock starts.
The most expensive habit in factory planning is writing phases as calendar periods. "Phase two in Q3" converts a technical decision into a deadline, and deadlines produce purchases that are justified by the date rather than by the evidence. The alternative is a condition: stage two starts when a measured number crosses a threshold that was written down in stage one, and the threshold is chosen so that the new stage has something to solve rather than something to fill.
Conditions have a second advantage that is easy to underestimate: they make the decision reversible. If the trigger has not fired, not building is a defensible answer, and nobody has to defend an underspend. If the trigger has fired, the evidence is already on the table and the conversation is about scope rather than about whether. In plants where phases are dates, the opposite happens — the equipment arrives, the justification is reconstructed afterwards, and the new section runs at whatever load the upstream process can feed it, which for a wave solder machine is the worst possible load profile.
Write the trigger as two numbers, not one. A single threshold invites gaming; a pair forces the reader to look at two different measurements. For through-hole the pair is insertion labour hours per week and hand-solder rework rate. For coating it is the share of the portfolio with a documented environmental requirement and the cleaning residue result on those products. For traceability it is the number of customer audits per year that ask for board-level records and the time currently spent retrieving a lot history by hand. Two numbers, both measurable from records you already keep, both reviewed on a fixed date.
Most of a factory can be changed. Six things cannot, or cannot without stopping production, and every one of them is decided in stage one by default — usually by omission rather than by choice.
The first is the floor plate: once conveyors are anchored to a slab and a coating room is built with a drained floor, the adjacency of the stages is fixed. The second is the electrical distribution board, which is sized once and then lives with that decision for twenty years; adding a feeder later means a shutdown and a new board. The third is the exhaust header route, because ducting that runs above a line cannot be re-routed without dismantling the line. The fourth is the compressed air main diameter, which is invisible until a second stage adds draw at the far end and every tool at that end starts starving. The fifth is the network topology, because a plant wired as a set of isolated line switches cannot feed an execution system without new cable runs through finished ceilings. The sixth is the identity strategy — whether a board gets its identifier at the loader or at the end of the line — because that single choice determines whether any later traceability stage can be built on existing process data or has to add a station in the middle of a working flow.
None of these six is expensive to get right in stage one. All of them are expensive to get wrong, and the cost does not appear in the stage that caused it. It appears two years later, in a project that was supposed to be an addition and turns out to be a rebuild.
Stage one is the only stage where you can spend a small amount of money to save a large amount later, and the money involved is almost never the equipment. It is the four interfaces the shell has to provide: floor area and its adjacency, electrical capacity, the air and exhaust stubs, and the data path. All four are cheap while the building is still being fitted out, all four are effectively fixed once the first line is anchored, and all four are invisible on the acceptance certificate. A stage one that passes its run-off test and leaves those four unresolved has passed the wrong test.
The framing worth holding onto is that stage one is not "a smaller version of the finished plant". It is a complete plant that happens to be missing three capabilities, and the interfaces are what keep it from being a closed system. Before any of this is scheduled, the site itself has to be closed out — the site readiness checks that close before phase one equipment lands cover the floor loading, the door clearances and the utility connections in the detail this article only summarises. What follows is the part that is specific to phasing: not whether the interfaces exist, but how much of them to build now. That distinction is the one a phased PCBA factory expansion plan exists to make explicit, because it is the only one that can be decided before the equipment is chosen.
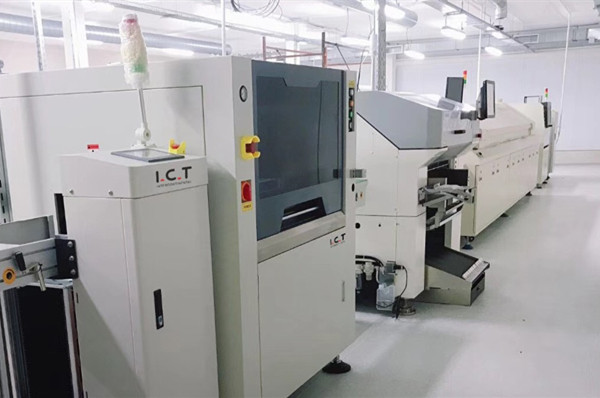
A single SMT line fits comfortably in a bay. Printing, placement, reflow, inspection and the board handling between them occupy a corridor roughly the length of the equipment plus the loading and unloading space at each end, and a hall that holds that corridor and nothing else will run perfectly well for two years. The problem is that a bay has walls, and a coating stage cannot live inside the same room as an SMT line without changing the pressure balance that the SMT line depends on.
So the floor plate decision is really a decision about whether the building can later be divided. Three arrangements are common and they differ in cost far more than they differ in convenience. The cheapest is a bay sized exactly for the first line, which means the second stage has to be built elsewhere in the building or in a new building. The middle option is a hall with the first line along one wall and clear span beside it, which allows the second stage to be added on the same slab but leaves the coating room to be built as a separate enclosure inside the hall. The most expensive at the outset, and the cheapest over ten years, is a hall designed from the start with three zones and a service corridor: SMT, then THT, then the wet zone, with the corridor carrying the exhaust, the air main and the cable tray to all three.
The numbers matter only as an illustration. If a single SMT line with its handling occupies roughly 220 m² and the three later stages need about 180 m² for through-hole, 120 m² for a coating room including its chemical store, and 60 m² for test and traceability stations, then the finished plant is in the region of 580 m² of productive floor. Deciding in stage one to lease 580 m² and fit out 220 of it costs very little more than leasing 220 and fitting it out — and it removes the single most common reason that a second stage gets delayed: there is nowhere to put it. Every one of those figures is an assumption for the purpose of showing the arithmetic, not a recommendation for a specific plant.
The distribution board is the clearest example of a stage-one decision that belongs to stage three. A board sized for the installed load of one SMT line will be full the day the line is connected, with perhaps one spare way for a future addition, and a coating line will need more than one spare way. Replacing a board means a shutdown of everything downstream of it, a new protection study, and in most jurisdictions a new inspection before re-energising.
Sizing for the last stage is not the same as buying transformers for equipment you have not ordered. It means buying the board, the busbar and the cable tray at the final rating while energising only the first stage's feeders. The practical method is to add the nameplate demand of each planned stage, apply a diversity factor once at the end rather than per stage, and then check the result against the board's rating. Using the assumptions above, an SMT stage of about 75 kVA, a through-hole stage of about 50 kVA and a coating stage of about 32 kVA come to roughly 157 kVA; at a diversity factor of 1.25 the board should be specified near 196 kVA even though only the first 75 kVA is connected today. The reason the standard matters here is scope: the scope that IEC 60204-1 sets for a machine group treats machines working together in a coordinated manner as one electrical system, starting at the point where supply connects — which is precisely why a board shared by three stages cannot be designed stage by stage.
Air and exhaust share a property that makes them the cheapest things to over-build and the most expensive things to extend: both are routed above the line and both are hidden by the ceiling once the fit-out is finished. A stage-one plant typically needs air for the printer, for nozzle cleaning and for a few hand tools, which is a modest draw. Adding through-hole brings fixture clamps and selective soldering; adding coating brings atomising air, which is a different quality requirement from the same main.
That quality question is where the purity classes in ISO 8573-1 earns its place in a phasing document. The standard defines purity classes for particles, water and oil independently of where in the system the air is specified or measured, which means a single main can serve both a shop-air class and a coating class as long as the final treatment is placed at the point of use — and it also means that a plant which never wrote down which class each stage needed will discover the mismatch at commissioning. Write the class per stage in the stage-one documents. It costs one line and prevents a dryer being retrofitted into a ceiling void.
The same logic applies to exhaust. A through-hole stage needs extraction at the soldering station. A coating stage needs an exhaust volume large enough to keep solvent concentration below the relevant limit and a make-up air path that replaces what is extracted without pressurising or depressurising the SMT hall. On the assumptions used here, an exhaust of roughly 3,000 m³/h with make-up at about 85% of that, carried in a duct sized near 250 mm, is a reasonable allowance — but the value of the allowance is not the figure. It is that the duct exists, capped, before the ceiling closes.
Stage one produces no traceability requirement in most plants, which is why the network gets designed as a convenience rather than as infrastructure. The line gets a switch so the machines can be programmed and the inspection station can store images, and that is the end of the thought. Two years later the plant wants board-level records, and discovers that the loader has no reader, the inspection systems store to local disks, and there is no path from the line to a server room that anyone thought to cable.
The fix is cheap and mostly documentary. Pull a cable tray along the same corridor as the exhaust and the air main, terminate more drops than stage one needs — somewhere in the region of 24 points across the hall is a reasonable planning allowance for three stages and a test area — and write down, per machine, what data it produces, in what format, and where it is stored. That last item is the one that saves the most money, because the traceability stage is not primarily a software purchase. It is a mapping exercise: which existing system already holds the record, and what is missing to join it to a serial number.
Interface | Stage 1 minimum | What to build now for later stages | Cost of doing it late |
|---|---|---|---|
Floor plate | Bay or hall sized for one line, roughly 220 m² | Lease and level the full productive area, around 580 m²; fix the three-zone adjacency before anchoring | Second stage moves to another building or waits |
Distribution board | Feeder for about 75 kVA | Board, busbar and tray rated near 196 kVA; energise stage one only | Board replacement plus shutdown and re-inspection |
Compressed air main | Draw for printer and hand tools | Main sized for about 2.2 m³/min total; point-of-use treatment for coating class | Ceiling void reopened; dryer retrofitted |
Exhaust header | None for a clean SMT line | Capped branch near 250 mm carried to the wet zone | Duct routed over a running line |
Network | Line switch and programming access | Tray plus about 24 terminated drops; per-machine data map | New cable through finished ceilings |
Identity point | None | Decide loader-side or end-of-line marking | Station inserted mid-flow, or no board-level records |
Read the table as a purchase order for the shell rather than for the line. Almost every row can be satisfied in stage one for the price of design attention and a modest amount of material, and almost every right-hand column describes work that has to happen while production continues. That asymmetry is the entire argument for phasing the interfaces rather than the equipment.

Through-hole is the stage that most often arrives as an emergency rather than a plan, because it is triggered by a product that was not in the original portfolio and a customer who will not wait. That is why it is worth deciding the design of the stage before the trigger fires: the trigger selects the timing, and the design should already be on the shelf. A stage planned in advance takes weeks to install; the same stage improvised takes months, and the difference is almost entirely in the interfaces that stage one either left or did not leave.
The engineering content of stage two is modest compared with stage three. Insertion is a people process with fixtures, soldering is a thermal process with exhaust, and inspection is a visual and X-ray question that depends on the joint type. What makes stage two difficult is that it is the first stage that interrupts a flow which was previously continuous, and it is the first stage that introduces a genuinely manual operation into a plant that until now was conveyor-fed. Both of those facts have to be handled at the boundary, and the boundary is where the money is.
The instinct is to put the new section wherever there is floor space, which is usually at the far end of the hall or in a corner vacated by something else. That instinct produces a plant where boards travel further than they need to and where the new section is permanently short of the handling it requires. The better rule is to place through-hole immediately after the SMT line's inspection point and before any test or depaneling step, because that is where the board is still a panel, still accompanied by its process record, and still moving in a direction that has not yet split into good and rework paths.
Two metres of conveyor is worth more than two hundred square metres of floor in this decision. If the sections are adjacent, a single operator can watch both, a single buffer can serve both, and a board that needs rework after soldering can re-enter the flow without a separate route. If they are at opposite ends of the building, every one of those three becomes a transport task with a person attached to it.
The placement also fixes ownership, which sounds like an organisational question and is actually a technical one. A section that physically belongs to the SMT area inherits the SMT area's discipline — the same first-article routine, the same changeover record, the same escalation path. A section in a separate room becomes its own island with its own habits within a quarter. If the plant has a documented interface matrix — the kind that names a single owner for each handoff between parties — this is the point where it gets used: who owns each interface between phases has to be answered for the SMT-to-THT handoff before the first board crosses it, not after the first dispute.
The soldering method is usually debated on quality grounds and decided on cost grounds, but its most durable consequence is the exhaust design. A wave machine carries a large open solder pot and a fluxer, so it needs extraction over its full length and a make-up air path that will not disturb the tunnel's thermal profile. A selective machine solders point by point under inert gas or with a local extraction hood, so it needs far less volume but far more local capture at the nozzle.
The choice should follow the board, not the budget. Wave suits panels with a high through-hole count concentrated on one side and a consistent orientation, where the wave can be masked to protect SMT parts on the underside. Selective suits mixed assemblies with connectors scattered across the panel, or where the through-hole content is small enough that a wave pot is a large idle mass of molten metal. The practical threshold is roughly whether insertion labour across the product family justifies a machine at all — which is exactly what the trigger numbers are for. On the assumptions used in this article, a single board carrying about 15 insertion points at roughly 3 s per point comes to around 45 s of direct labour per board; at volumes where that reaches about 120 h per week, or where hand-solder rework on through-hole joints exceeds about 2%, the case for a machine is no longer marginal.
Whichever method is chosen, size the exhaust for the larger of the two and install the branch in stage one. The difference in duct diameter between a wave and a selective installation is not large, but the difference between having a capped branch and having none is the difference between a two-week installation and a six-week one.
Every through-hole stage generates a physical inventory that no equipment quotation mentions. Insertion fixtures, solder pallets, masking plates, lead-forming tools and the racks that hold them are product-specific, they accumulate with the portfolio, and they need to be stored close enough to the line that changeover does not become a walk. A plant that installs a soldering machine and no fixture storage discovers within a month that pallets are stacked on the floor beside the line, which is both a quality risk and a changeover bottleneck.
The planning allowance is straightforward once you accept it: one pallet or fixture set per active product, plus the sets currently in the wash or in repair, plus a margin for the products that will be added. That is a storage volume, not a shelf, and it belongs in the stage-two floor plan next to the machine rather than in a store room two doors away. It also needs a cleaning path, because solder pallets accumulate flux and a pallet that is not cleaned becomes a defect source that is very hard to trace back to its cause.
There is a second-order effect worth naming. Fixtures are where the through-hole stage's process knowledge physically lives — the mask opening that prevented bridging, the support post added to stop a connector tilting. A plant that stores them without identification loses that knowledge at every changeover and re-solves the same problem on the next run. Identification is cheap and belongs in stage two, not in the traceability stage.
The interface between a conveyor-fed SMT line and a people-fed insertion section is a rate mismatch, and rate mismatches are absorbed either by a buffer or by stopping. Without a buffer, the SMT line stops whenever insertion falls behind, and insertion idles whenever the SMT line is changing over. With a buffer of even a few panels, the two sections decouple enough that each can run at its own rhythm for the length of the buffer, which is usually all that is needed.
Sizing the buffer is a small calculation with a large effect. Take the SMT line's cycle time per panel and the insertion section's cycle time per panel; the difference is the drift rate. Multiply by the changeover duration and you have the number of panels the buffer must hold to cover a changeover without stopping the upstream line. In most mixed-technology plants that lands somewhere between a few panels and a few dozen, which is one conveyor section with accumulation rather than a separate machine.
The buffer also has a quality function that is easy to miss. It is the physical place where a panel waits between two processes, which makes it the natural place to hold a panel that has been flagged — ahead of soldering rather than after it. A plant with no buffer has nowhere to put a suspect panel except back on the line or on a bench, and both of those turn a controlled hold into an uncontrolled one.
Decision | What it fixes | Reversible later? | Where it belongs |
|---|---|---|---|
Location of the THT section | Transport, shared supervision, rework route | No — conveyors are anchored | Stage 1 layout |
Soldering method | Exhaust volume, make-up air, floor load | Partly — branch can be oversized early | Stage 1 exhaust stub, stage 2 machine |
Fixture storage | Changeover time, defect traceability | Yes, at the cost of floor space | Stage 2 floor plan |
Inter-section buffer | Whether either section ever has to stop for the other | Yes, but expensive once conveyors are fixed | Stage 1 conveyor layout |
Handoff ownership | Who answers for a defect found after the boundary | Yes, but only on paper | Before the first board crosses |
Notice how many rows land in stage one. That is the recurring pattern of phased building: the decisions that make stage two cheap are made before stage two exists, and the decisions made during stage two are mostly about which machine to buy.
Stages one and two add equipment to a building. Stage three adds a building to a building. A coating room is a wet process with a chemical store, an exhaust system, a cure path and a controlled access boundary, and every one of those has to exist before the first board is coated. This is the stage where the phrase "we will find room for it" stops being true, and it is the stage that most often causes a plant to renegotiate a lease it thought was settled.
Cleaning sits alongside coating because the order between them is fixed by chemistry rather than by preference: you cannot coat over residue and expect the coating to adhere. Whether a plant needs an inline cleaner, a batch cleaner or none at all depends on the flux chemistry and the product's cleanliness requirement, and that decision is upstream of the coating decision. A plant that installs a coater without settling the cleaning question will discover the answer through adhesion failures, which are among the most difficult defects to diagnose after the fact.
The phrase "we can always put the coater in the corner later" survives because coating equipment itself is compact. A selective coating machine occupies less floor than a printer. What the phrase ignores is everything the machine needs in order to be legal and repeatable: a room with a drained and bunded floor, a fire-rated chemical store for solvent, an exhaust connection sized for the solvent load, a make-up air path that does not depressurise the adjacent SMT hall, and a cure area with enough travel that wet boards are not handled before they are dry.
Retrofitting those into a corner means building a room inside an operating hall, which means dust, noise and restricted access for the duration, and it means routing exhaust ducting across a ceiling that is already full. In a plant that has been running for two years, the exhaust header may no longer have spare capacity, the electrical board may have no spare ways, and the compressed air main may be at its pressure limit at the far end. Every one of those is a stage-one item appearing as a stage-three invoice.
The practical test is simple. If the answer to "where does the exhaust go" is a blank look, the corner is not available. If the answer is a capped branch installed two years ago, the corner has been waiting.
Three spaces are needed and only one of them contains the machine. The application room holds the coater and the operator; it needs the extraction, the lighting for inspection and enough clear floor to lay out boards for masking. The chemical store holds the coating material, the solvent and the masking consumables, and it needs to be separate, bunded and ventilated, because the material that makes coating effective is also the material that makes it a fire risk. The cure path is the space where boards sit while the coating reaches its handling strength, and it is the space most often forgotten.
The cure path is not a shelf. Coating cure is a time-and-temperature process, and boards that are moved too early smear, bridge and lose the coverage the process was installed to provide. On the assumptions used in this article, a coating room of about 120 m² including its store is a reasonable planning allowance for a single selective coater with a cure area and a masking bench — but the important part is the relationship: the cure area should be between the coater and the inspection point so that no wet board is ever carried across a walkway.
Ventilation for the room is usually specified as air changes per hour rather than as a flow, because the requirement is to keep solvent concentration below a limit regardless of room size. A figure in the region of 12 air changes per hour appears in many plant specifications for a coating room, and it is worth writing down as an assumption in stage one even though the final number belongs to the safety assessment.
The interaction that catches most plants is not the coating room's own exhaust, it is what that exhaust does to the room next door. Extracting a large volume from a small room creates a negative pressure that pulls air through every gap in the partition, and if the adjacent space is the SMT hall, the hall's pressure drops, its own exhaust becomes less effective, and flux vapour that used to leave now stays. The symptom appears as a rise in solder-related defects that nobody connects to the coating installation.
The countermeasure is to supply make-up air deliberately rather than letting the room find it. Supplying at roughly 85% of the extracted volume keeps the coating room slightly negative relative to the SMT hall, which is what you want — contaminants should flow into the wet room, not out of it — while limiting the disturbance to the neighbouring space. On the assumptions here, an exhaust near 3,000 m³/h with make-up at about 85% of it, carried in a duct around 250 mm, is a workable starting point for a single coater with a masking bench.
Balance the system with the SMT line running, not with the plant empty. A plant that commissions its coating exhaust on a quiet weekend will find the balance has changed on Monday, when every reflow oven and every extraction hood in the hall is drawing at the same time. Commissioning the balance under production load is the only measurement that means anything.
Where the product is an LED assembly, this whole calculation arrives earlier than in most plants, because the service environment is the reason the product exists: the LED line where coating is scoped from day one treats the wet room as part of the line rather than as an addition to it, and the exhaust and cure path are sized with the placement and reflow equipment instead of after it.
Coating is a process where the labour is not in the coating. Applying the material takes seconds per board; masking the connectors, test points and board edges that must stay uncovered takes minutes. Masking is also the step most likely to be under-estimated in a business case, because it is invisible on an equipment quotation and it scales with the number of masked features rather than with the number of boards.
The decision to automate masking — with a dispense robot, a masking fixture or a peelable resist — is therefore a labour calculation, and it has a clean break-even structure. Count the masked features per board, multiply by the handling time per feature, multiply by the annual volume, and compare the result with the cost of the automated option amortised over its life. In plants with many masked features per board the automated option wins quickly; in plants with two connectors per board it never wins, and the right answer is a better masking fixture rather than a robot.
Two related numbers belong in the same calculation and are usually left out. The first is the rework cost of a masking escape, which is a coating removal and re-application on a finished assembly. The second is the cost of cleaning residue that was not removed before coating, which only shows up as an adhesion failure weeks later. Both push the decision toward doing the masking properly rather than quickly, which in practice means a fixture and a trained operator before it means a robot.

Traceability is the stage that everybody agrees with and nobody schedules, because it produces no boards and its benefits are invisible until something fails. It is also the stage most sensitive to decisions made years earlier, since the only economical way to build it is to attach records to processes that already exist. A plant that instruments its processes from stage one can build traceability with marking stations and a data model. A plant that did not has to add data capture to processes that were designed without a place to put it.
The good news is that the standard is unusually clear about how much traceability a plant needs. It is not a fixed specification that everyone must meet; it is a risk-based level chosen by the parties. That framing matters for phasing because it lets a plant move up a level as its customer base changes, instead of buying the highest level on day one and using a fraction of it. In a phased PCBA factory expansion plan, traceability is therefore a stage with a defined level attached to it, not a system that arrives in a box.
IPC-1782 and its four traceability levels is the reference most electronics plants end up using, and its structure is worth understanding before any budget is set. The standard's minimum requirements are not a single specification: as the published description puts it, minimum requirements are based on four levels of traceability for materials and processes, and those levels can be correlated to the IPC product classification system or to the business model of the end market. In other words, the level is a consequence of what the product has to prove, not of how modern the factory wants to look.
The honest way to choose is to work backwards from a failure. Ask what the plant would have to produce if a customer reported a field failure on a board shipped eight months ago. If the answer is a lot number and a date, level one or two is the requirement. If the answer is the specific component reel, the program version, the inspection images and the rework history for that serial number, the requirement is higher, and no amount of software will substitute for processes that never captured those facts.
This is also where the risk-based approach IPC-1782 takes earns its keep in a phasing document. Because the level follows perceived risk as agreed between user and supplier, a plant can legitimately run a consumer product line at a lot-level requirement and a different product at serial level, and it can change that judgment when the customer base changes. That is a phased answer to a question usually answered once and regretted.
Every traceability system rests on one physical fact: at some point a board receives an identifier, and everything downstream refers to it. That point is chosen once. Marking at the loader means the identifier exists before the first process, so printing, placement and reflow can all be bound to it without adding a station later. Marking at the end of the line means the identifier is created after the processes it is supposed to describe, which makes it impossible to bind process data to the board and leaves only lot-level records.
There is a legitimate reason to mark late: laser marking on a finished assembly risks damaging what it describes, and some board surfaces do not accept a mark cleanly. Where that is the case, the identifier can be created at the loader as a label rather than a laser mark, and the label removed before coating if the product does not permit it. What is not legitimate is failing to decide, because the default outcome is late marking by accident, discovered when someone finally asks for board-level records.
The cost of getting this right in stage one is small: a marking or labelling station at the loader, a reader at each inspection point, and the network drops that connect them. The cost of getting it wrong is a station inserted in the middle of a working flow, which usually means a conveyor reconfiguration.
Traceability does not arrive as one system; it accumulates as a set of records, and each stage of the build adds records that later stages depend on. Writing that list down at each stage is what turns traceability from a purchase into a by-product.
Stage one contributes the SMT records: stencil and paste lot, printer parameters, placement program version and feeder setup, reflow profile identifier, and the inspection results from SPI and AOI. Stage two adds the through-hole records: insertion station, fixture identifier, soldering method and its parameters, post-solder inspection result and any touch-up with its reason. Stage three adds the coating records: material lot, viscosity or batch verification, application parameters, cure time and temperature, and the inspection result including coverage. Stage four is where all of it is joined — not by re-entering it, but by binding existing records to the identifier.
The test of whether a stage has produced its records is whether the record can be retrieved without asking a person. A profile identifier that lives in an operator's notebook is not a record; a profile identifier stored in the oven's controller and reachable over the network is. Applying that test at each stage is cheaper than applying it once at the end, because at the end every gap becomes a project.
Manufacturing execution systems are sold as the answer to traceability, and they are — for the joining layer. They are not the answer to missing data, and the most common failure in this stage is buying the system before the records exist. A plant that installs an execution system on processes with no data capture gets a very expensive dashboard showing that nothing is being captured.
The split is worth stating plainly. What cannot wait is identity: the marking point, the readers and the storage of the records each process already produces. What can wait is orchestration: enforcement of scan-before-run rules, real-time dashboards, work-order routing, and integration with planning systems. The first is a few marking stations and a great deal of discipline in choosing what each machine logs. The second is a project with a vendor, a schedule and a budget that belongs in stage five.
A useful sizing check before committing to the orchestration layer is whether the manual equivalent already works. If a plant can retrieve a board's history by hand in under an hour, the process is defined and the system will automate it. If retrieving the same history requires walking the floor and asking three people, the system will encode that confusion rather than resolve it. On the assumptions used here, a marking station with a reader at roughly USD 12,000 is a stage-four purchase, while an execution system in the region of USD 45,000 in its first year is a stage-five one — and the cheaper item is the one the later item depends on.
Where the product is a high-volume consumer assembly rather than an industrial one, the level question often answers itself. A set-top-box line where lot-level records are enough is a perfectly defensible position under a risk-based standard, and it is a much cheaper position than serial-level tracking on a product that will never generate a field-failure investigation. The mistake is not choosing a low level. The mistake is choosing a high level for one product and then applying it to everything because the system was bought for the whole plant.
The last stage is the one that gets planned first and built last, which is why it accumulates the most deferred work. Automation and execution systems are attractive to approve because they promise measurable labour and visibility gains, and they are easy to defer because neither produces a board. The result is that by the time they are funded, the plant has four stages of habit built around manual handling, and the automation project becomes an exercise in fitting machines into a flow that was never designed to accept them.
There is a way to avoid that, and it is not to buy automation early. It is to keep the three retrofits that automation depends on cheap by making them part of stage one. Everything in this stage — loaders, unloaders, closed-loop inspection, scan-before-run enforcement — needs the same three things: floor space at the ends of the line, network connectivity to every station, and a board identity that exists before the first process. All three are stage-one decisions. The machines themselves are not.
The first is board loading and unloading. A line that starts with manual loading is perfectly viable, and the manual loader is often the right choice while volume is uncertain. What is not viable is a line whose entry and exit were designed with no room for an automatic loader, because the automatic loader arrives with a magazine handler, a footprint and a reach requirement that has to sit exactly where the operator's bench was. Reserving the floor at both ends costs nothing in stage one and saves a conveyor reconfiguration later.
The second is network and control connectivity at every station, including the ones that do not need it yet. Automation in this industry increasingly means machines talking to each other and to a plant system, and the interface standards that make that possible all assume a network connection at the machine. A plant that wired its line as isolated switches has to run cable before it can run any integration project, and running cable through a finished ceiling over a running line is the definition of brutal.
The third is board identity, already covered in stage four, but worth repeating here because automation depends on it more than traceability does. A scan-before-run rule, an automated rework route, a closed-loop inspection decision — each of them needs to know which board it is looking at. Where the product is a high-volume consumer board, the automation often arrives as a complete line rather than as retrofits: a fully automatic STB line where board loading is already closed is scoped that way from the start, and the point of mentioning it here is that the scoping decision, not the machine list, is what a phased plant has to get right in stage one.
Automation decisions are usually argued from labour cost and decided from capital availability. A trigger written as two numbers replaces that argument with a measurement, and the numbers can be derived from records the plant already keeps.
The first pair belongs to loading and unloading: operator hours per shift spent moving magazines, and the number of times per shift the line stops waiting for boards. If both are rising while volume is flat, the constraint is handling rather than process, and no amount of placement speed will help. The second pair belongs to inspection feedback: the share of defects detected after the process that caused them, and the average time between a defect occurring and the line being adjusted. If defects are being caught at the end of the line and the adjustment happens the next shift, the loop is open and automation of the feedback path has a measurable return.
The third pair belongs to changeover, and it is the one most often mismeasured. Count the time from last good board of product A to first good board of product B, and count how much of that time is spent on tasks that require a person to read something and type it. The typing portion is the automatable portion, and it is often the majority in plants with many product families. Neither number requires new equipment to collect; both require someone to stand with a stopwatch for a week, which is why they rarely exist.
An execution system is a joining layer, and joining requires two things at every process: a record that exists, and an identifier to join it to. Everything else the system does — dashboards, routing, enforcement — is built on those two. This is why the honest prerequisite list for an MES project contains no software items at all.
The list is: every process stores its result somewhere retrievable; every stored result carries the board or lot identifier; the identifier is created before the first process; and the network reaches every station that stores something. A plant that can answer yes to those four will implement an execution system in months. A plant that cannot will spend the same months building those four things while the software waits, and will usually conclude that the software was the problem.
There is a useful intermediate step that costs little and de-risks the whole stage: instrument one line completely before buying anything for the plant. Choose the line with the most customer scrutiny, make every one of its processes store a retrievable record against the identifier, and prove the retrieval works by asking someone who did not build it to produce a board history. What that exercise reveals — usually two or three processes that store nothing, and a marking station in the wrong place — is the actual scope of the plant-wide project.
Everything above reduces to a single document that a plant either has or does not: a one-page schedule of what the shell must provide now so that later stages cost less. It is not a capital plan and it is not a layout drawing. It is the list of things that are cheap before the first conveyor is anchored and expensive after, with a number against each one. It is also the page that turns a phased PCBA factory expansion plan into something a finance committee can approve, because every line on it has a price and an alternative.
The reason this document is rare is that it crosses departmental boundaries. The floor area belongs to facilities, the electrical capacity to the electrical contractor, the air and exhaust to mechanical, the network to IT, and the identity decision to production. Nobody owns the whole list, so nobody writes it, and each department optimises its own scope against a budget that will not survive contact with the next stage. Writing the list is the cheapest coordination mechanism available.
Take a plant planning three stages on one slab: an SMT line today, a through-hole section in two years, a coating room when a product requires it. The arithmetic below is an assumption set built to demonstrate the method, not a quotation or a measurement from any project.
Power first, because it is the least reversible. An SMT stage around 75 kVA, a through-hole stage around 50 kVA and a coating stage around 32 kVA total about 157 kVA of connected demand. Applying a diversity factor of 1.25 to the total rather than to each stage gives roughly 196 kVA, and that is the number the board, the busbar and the cable tray should be rated for. Stage one energises only its own feeder. Floor next: about 220 m² for the SMT stage, 180 m² for through-hole, 120 m² for the coating room and its store, and 60 m² for test and traceability stations give approximately 580 m² of productive area, of which stage one fits out a little over a third.
Services next. Compressed air at roughly 2.2 m³/min across the three stages, with point-of-use treatment for the coating class. An exhaust branch near 250 mm carried to the wet zone and capped, sized for the larger of a wave or selective installation. A cable tray along the same corridor with around 24 terminated network points. And one non-physical item that belongs on the same page: the identity decision, written as a sentence, loader-side or end-of-line.
The figures are illustrative, and a real plant will arrive at different ones. What does not change is the shape of the document: one row per interface, one number per row, and a column stating which stage pays for it. Once that column exists, the argument about whether to spend in stage one becomes a comparison of two numbers instead of a difference of opinion.
Interface | Number to reserve | Paid by | If deferred to the stage that needs it |
|---|---|---|---|
Distribution board and busbar rating | 196 kVA total, 75 kVA energised | Stage 1 | Board replacement, shutdown, re-inspection |
Productive floor area | 580 m² leased, 220 m² fitted out | Stage 1 | Second stage relocated or postponed |
Compressed air main | 2.2 m³/min capacity, coating-class treatment at point of use | Stage 1 main, stage 3 treatment | Ceiling reopened, dryer retrofitted |
Exhaust branch to wet zone | 250 mm, capped | Stage 1 | Duct routed over a running line |
Network tray and drops | 24 points | Stage 1 | New cable through finished ceilings |
Board identity point | Decision recorded, station installed | Stage 1 decision, stage 4 station | No board-level records, or a station mid-flow |
Two columns carry the weight. The number column is what the contractor builds to, and the "paid by" column is the one that prevents the schedule from being renegotiated every budget cycle. A reservation that has no owner and no funding line is not a reservation; it is a note. Keep the schedule to one page, print it into the stage-one design documents, and treat any change to it as a scope change with a cost attached rather than an adjustment of taste.
A reservation schedule only works if the money follows the same logic. Most capital plans phase by equipment because equipment is what appears on a purchase order, and the shell work gets absorbed into whichever stage happens to be spending that year. The result is that the cheap stage-one items are deferred to the expensive later stages, which is precisely backwards.
The fix is to phase by interface rather than by asset. Stage one carries the shell items whose cost rises with delay: the board rating, the slab and the zones, the capped branches, the tray. Stage two carries equipment and fixtures. Stage three carries the room, the extraction and the cure path, plus the point-of-use treatment that the air main was sized for. Stage four carries marking stations and readers. Stage five carries software and the machines that depend on everything before them.
There is a useful way to test whether a plant has done this properly. Ask what the next stage would cost if it started tomorrow with no building work. If the answer is close to the equipment price, the interfaces were reserved. If the answer is a multiple of the equipment price, they were not, and the difference is the invoice for a decision that was never made.
The cost of a missing interface is not theoretical. In one engineering case from our own project records, a newly built SMT hall for mobile-phone mainboards had its walls and floor finished before the electrical distribution, compressed air and reflow exhaust were ready. The line arrived on schedule; commissioning did not. The site report lists what had to be resolved in sequence: cable, breaker and distribution-board recommendations had to be issued before anything could be energised; voltage instability then tripped the line, stopped the compressor and heated the reflow oven's incoming feeder; a temporary compressor could not carry the whole line at once, so a new compressor, receiver, dryer and pipe run were installed mid-project; and the reflow exhaust duct had to be braced with additional cross members because the original support flexed under load. The project consumed 34.5 days of on-site engineering support, according to I.C.T project records. None of those four items was a machine fault. Each one was an interface that belonged to an earlier phase and had been left for the stage that needed it.
That is the whole argument in one case. Reserving an interface costs design attention and a modest amount of material while the building is open. Not reserving it costs a commissioning sequence that nobody planned, in a plant that is already committed to a delivery date. The sequencing risk of each stage can be scored before the money is committed — the phase-sequenced risk register that scores each stage sets out how to rank those items by cost rather than by opinion.
For plants that would rather buy the whole sequence as one scope, the alternative to a reservation schedule is a single contract that includes all five stages from the outset. That is a legitimate choice and it is what a turnkey drone line that arrives with all five stages already scoped represents — but note what makes it work: the interfaces are decided once, at the start, by someone who can see the end state. Whether that is done with one contract or with a schedule and three budget cycles matters far less than whether it is done at all.
Bring us your phase one plan and we will tell you what it costs to add phase three
Send us the product mix you expect in year one and the products you expect to quote in year three, together with the building dimensions and the utility capacity you have today. We will map the five stages onto your floor, mark which interfaces have to be closed before the first conveyor is anchored, and give you a reservation schedule with the numbers that belong in your capital request rather than in a vendor's brochure. Send what you have; a rough layout sketch and a single-line electrical diagram are enough to start.
What we will not do is quote you a finished five-stage plant for a stage-one budget. The useful output of this exercise is a plan where stopping after any stage still leaves a working factory, and where the next stage costs close to its equipment price instead of a multiple of it. That distinction is the whole point of building in phases, and it is decided in the first four weeks, long before any machine is ordered or any lease is signed.
Yes, and many plants do it first. Hand soldering with a trained operator and a proper fixture is a legitimate way to serve a small through-hole content, and it generates the labour data you need to justify a machine later. The limitation is repeatability rather than capability: hand-soldered joints depend on the operator, so the rework rate becomes the number to watch. When that rate stays above roughly 2% on a stable product, or when insertion labour crosses about 120 hours per week, the case for selective soldering is no longer marginal. What you cannot skip is the fixture and the post-solder inspection, because those are what make the process definable at all.
Reserve the productive area, fit out only what stage one needs, and make the reserve a lease condition rather than an intention. As an illustration, a single SMT line with its handling occupies roughly 220 m², a through-hole section about 180 m², a coating room with its chemical store about 120 m², and test and traceability stations about 60 m², which totals approximately 580 m². Leasing that area and fitting out a third of it costs very little more than leasing a third, and it removes the most common cause of a delayed second stage. The number that matters is not the total but the adjacency: the three zones and the service corridor have to be fixed before the first conveyor is anchored.
No, and the order is usually the other way round. Traceability rests on two things: a board identifier created before the first process, and every process storing a retrievable record against that identifier. An execution system joins those records together and automates the enforcement; it cannot create records that were never captured. A plant that installs the software first typically spends the implementation period building the data capture it should have built first, and then concludes the software was at fault. Instrument one line completely, prove that someone who did not build it can retrieve a board history, and only then scope the plant-wide system.
Build the interfaces early; build the room when a product requires it. The interfaces are the exhaust branch to the wet zone, the make-up air capacity, the electrical ways on the board and the floor area with a drain and bund. Those cost little while the building is open and a great deal once a ceiling is closed and a line is running. The room itself, its extraction and its cure path are a capital item that should follow a documented environmental requirement rather than precede it. A plant that builds the room speculatively usually ends up with a clean room holding a coater that runs one product family, while the money that would have secured the interfaces was spent on the enclosure.
It depends on the product, which is exactly what a risk-based standard is designed to handle. IPC-1782 bases its minimum requirements on four levels of traceability for materials and processes, and its framing ties those levels to the product classification and the end market rather than to a single plant-wide specification. In practice, work backwards from a failure: ask what you would have to produce if a customer reported a field failure eight months after shipment. A lot number and a date is a defensible answer for many consumer products. Specific component reels, program versions and inspection images for one serial number is a different answer, and it belongs to a different product line. Choosing different levels per product family is legitimate and usually cheaper than choosing the highest level for everything.
Write two numbers into the stage-one plan and review them on a fixed date. The first is insertion labour hours per week across the through-hole product family; the second is the hand-solder rework rate on through-hole joints. On the assumptions used in this article, a board carrying about 15 insertion points at roughly 3 seconds per point comes to around 45 seconds of direct labour per board, so the weekly hours follow directly from volume. When that figure reaches about 120 hours per week, or the rework rate passes about 2%, the machine decision has evidence behind it. Until then, not buying is the defensible answer, and having the numbers is what makes it defensible without an argument.
Physical additions can almost always be done alongside production; the stopping happens when an interface has to be replaced rather than extended. Adding a machine, a conveyor section or a coating room inside an existing hall is disruptive but schedulable around shifts. Replacing a distribution board, re-routing an exhaust header or pulling new cable through a finished ceiling requires the affected line to be down, and the duration is measured in days rather than hours. That asymmetry is the reason the reservation schedule exists: it converts shutdown work into extension work by paying for capacity before it is needed. A plant that oversized its board, its air main and its duct route in stage one can add three stages without a single unplanned shutdown.