English
Views: 0 Author: Elsa Long Publish Time: 2026-11-16 Origin: Site


A turnkey quotation usually arrives as one number, and that single number is the reason projects stall. The number covers equipment, but the boundary it draws is invisible: whether the exhaust duct is included, whether the compressed air drop is capped at the machine or run back to the compressor, whether the MES interface is a data tag or a working handshake, whether the operators are trained at the factory or on site, and whether the spare parts list is a recommendation or a contractual first stock. Each of those is a decision worth real money, and each one is normally made by accident because nobody wrote it down. A turnkey PCBA factory scope of supply checklist exists to convert that single number back into twelve boundaries that can be argued about on paper rather than on site, three months into installation.
This guide is written for the buyer side of that conversation. It assumes the process route is already decided — whether the plant is SMT only, SMT with through-hole, or SMT with coating is the upstream question, and it changes which blocks even exist. What follows is how to write the boundary itself: the twelve supply blocks, the three columns each line item needs, the utility handover points that cause most disputes, the exclusions that should never be left implicit, and a worked matrix you can fill in before the RFQ goes out. The equipment behind the SMT block is packaged in the line packages that make up the SMT block; here the line is treated as one item in a larger list, because the larger list is what the contract is actually about.
A machine list answers "what will be installed". A scope document answers four different questions: what is delivered, what is installed, what is connected, and what is handed over. Those are separate obligations, and the same sentence in a quotation can mean any of them. "Reflow oven included" might mean a crate on a truck, a machine on its feet with power connected, a machine running at temperature with a profile signed off, or all three plus a spare heating zone. The difference between the first and the last interpretation is routinely a five-figure sum and several weeks of schedule. Writing a turnkey PCBA factory scope of supply checklist is therefore not administrative work that happens after the technical decision; it is the technical decision, expressed in a form that a contract can hold. The method below takes about two days for a mid-size project and prevents the argument that otherwise arrives during commissioning.
Machine lists are organized by equipment, and equipment is the least ambiguous part of a project. A placement platform is a known object with a datasheet, a footprint and a price. What surrounds it is not: the duct that has to reach it, the air drop that has to be at pressure when it arrives, the operator who has to be able to change a feeder, the program that has to exist before the first product runs. None of that appears in a machine list, and all of it appears in the critical path. A scope organized by equipment therefore looks complete while leaving the majority of the interface work unassigned. The practical fix is to organize the same project by function instead — the twelve blocks in the next section — and to record, for each block, whether the deliverable is equipment, installation, connection, training or documentation. Same content, different axis, and the axis is what exposes the gaps.
Every line in the scope should carry three columns, and the third is the one people skip. Column one is in scope: what the supplier delivers, described as an object with a quantity and a condition. Column two is out of scope: what the supplier explicitly does not deliver, written positively rather than implied. Column three is the interface: the physical or logical point where the two sides meet, described precisely enough that a third party could verify it. "Electrical: supplier" is not a scope line. "Supplier provides a control cabinet with a 5-metre flying lead terminated in a 32 A three-phase plug; buyer provides a socket within 5 metres of the cabinet position, energised before the agreed installation date" is a scope line, because it names the object, the boundary and the condition. The test for a finished line is simple: could two people who have never spoken to each other read this row and agree on who buys the cable? If not, the row is not finished, whatever else the document contains.
Most delays at the end of a factory project are not equipment failures. They are unassigned interfaces: a duct that reaches the ceiling but not the stack, a network drop that exists but terminates in the wrong room, a floor that carries the machine but not the loaded pallet in front of it, a compressed air line that is installed but not dried. The reason is structural. Interfaces sit between two scopes, and each side reasonably assumes the other covers the last metre. Writing them down has a second benefit beyond allocation: it forces a dimensional check. An interface that has to be described as "duct flange at 2,400 mm above finished floor, 400 mm from the wall" gets measured, and measuring it is what reveals that the ceiling beam is in the way. Factories that complete their scope document before RFQ consistently report fewer site variations, and the mechanism is not contractual discipline — it is that the drawing had to be looked at.
Turnkey is a delivery model, not a legal guarantee of completeness. In practice it means one counterparty takes responsibility for integrating the blocks it supplies and for commissioning them to an agreed output. It does not automatically mean that civil works are included, that utilities are brought to the machines, that permits are obtained, that local labour is trained to competency, or that a first stock of spares sits on the shelf. Those items are frequently outside the turnkey envelope, and they are frequently assumed to be inside it. The honest way to use the word is to attach it to a defined boundary: "turnkey supply and commissioning of the twelve blocks listed in Appendix A, excluding civil works, utility supply beyond the points in Appendix B, and statutory permits". That sentence is worth more than any amount of reassurance, because it can be checked against an invoice, and an invoice is the one document every project eventually has to reconcile.
The twelve blocks below cover a complete PCBA plant, and the list is deliberately functional rather than equipment-based so that nothing falls between categories. Not every project includes all twelve: a plant that runs SMT only has no DIP block and no coating block, and a plant that buys boards from a subcontractor has no warehousing block in the same sense. Which blocks exist is set by the route decision, which is why the route decision that decides which blocks exist at all should be recorded in the same document, one page ahead of the scope. The table gives the default owner for each block and the point that most often becomes a dispute. Default is not destiny — any block can move — but a project that deviates from the default in more than two or three places should say why, in writing, because the deviations are where the cost concentrates.
Block | Default owner | Where the dispute usually lands |
|---|---|---|
1. SMT process equipment | Supplier | Whether loading and unloading automation is in the package or an option |
2. DIP / THT section | Supplier for machines, buyer for manual stations | Whether the belt assembly line and post-solder inspection are inside the line price |
3. Cleaning | Supplier if specified, otherwise absent | Water supply, drain and waste treatment are almost always buyer side |
4. Coating | Supplier for applicator and cure, buyer for the room | Whether the enclosure, extraction and chemical storage form part of the scope |
5. Inspection | Supplier | Which inspection points are inline versus offline, and who defines the defect library |
6. Traceability hardware | Supplier | Marking, reading and the label standard the buyer's customers will accept |
7. MES and data | Shared, and therefore the riskiest | Whether the interface is a data tag or a working two-way handshake |
8. Warehousing and material handling | Buyer | Feeders, carts, racks and stock location are usually omitted from both sides |
9. Utilities and civil works | Buyer | The last metre from the building service to the machine |
10. Training | Supplier | Hours, language, location and what counts as proof of competence |
11. Spare parts | Supplier for the first package, buyer thereafter | Whether the list is a recommendation or a committed stock with lead times |
12. Documentation | Supplier | Language, format, revision control and whether editable files are included |
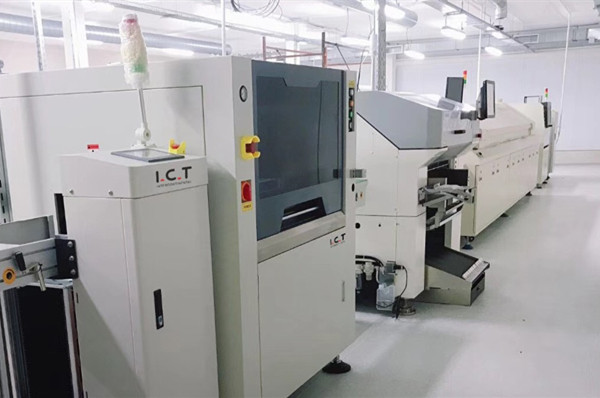
The four process blocks are the ones a buyer naturally focuses on, and they are also the ones where the internal boundary matters most. In the SMT block, the question is where the package stops: printer, mounter and reflow are the core, but loader, unloader, buffer, SPI and AOI are frequently optional, and the price difference between a core package and a fully automated one is large. A starting project with an unsettled mix can reasonably take a flexible semi-automatic SMD line and add automation as the mix stabilizes; what it should not do is assume the automation will be added later without a floor and a duct provision. In the DIP block the same question appears as stations rather than options, and the cleanest way to scope it is to buy a DIP section scoped as a complete line, not a single machine, then remove the stations you are postponing by name. Cleaning and coating are the two blocks most often absent from the quotation entirely, which is why they should be written as either included or excluded, never left silent.
Inspection scope has a habit of expanding after the first production trial, because defect escape is discovered late and the answer is usually another inspection point. Write the inspection block with three explicit settings: the points that are inline and permanent, the points that are offline and sampled, and the criteria that decide when an offline point becomes inline. Traceability is the same problem in a different form. The hardware — a laser marker, a reader, a label printer — is easy to scope. The rules are not: which side of the board is marked, what the code format is, how long records are retained, and whether the buyer's customers require a specific identifier scheme. A traceability block that specifies hardware and omits rules will be rebuilt within a year, usually at the buyer's cost, because the hardware was delivered correctly and the rules were never agreed — a failure of specification rather than of supply, and one that no amount of goodwill can fix afterwards.
The MES block is the single most common source of post-installation dispute, and the reason is that it has no natural owner. An equipment supplier can deliver a machine that exposes data; it cannot deliver a working manufacturing execution system for a factory it does not run. A software vendor can deliver an MES; it cannot make a twenty-year-old oven report parameters it never exposed. So the block has to be split explicitly into three parts: the data that each machine exposes and in what protocol, the middleware or gateway that collects it, and the system of record that consumes it. Write all three, name the owner of each, and specify the acceptance test as a data point observed in the consuming system rather than a port that exists on the machine. A scope that says "MES-ready" has specified nothing. A scope that says "cycle time, status and alarm code for each station visible in the buyer's MES within 30 days of handover" has specified a deliverable.
This block is almost always omitted by both sides, and it is the one that stops a line from running. Feeders are the classic case: a placement platform arrives with a feeder count that matches the quotation, and the quotation matched the sample product rather than the product family. The second product needs a different feeder mix, which is a purchase nobody planned. Around the machine, the same pattern repeats with carts, racks, magazines, stencils, squeegees and stock locations. The scoping method is to build the block from the product family rather than from the machine: list every consumable and carrier that has to exist for each product to run, multiply by the number of products that will run concurrently, and mark each item as machine-supplied, buyer-supplied or to be decided. That last category is the useful one, because it is where the RFQ should ask a question instead of assuming an answer. A row marked "to be decided" is not a gap in the matrix; it is a question with a name attached to it, and questions with names get answered before the order rather than during installation.

Utilities are where a turnkey project most often turns into two projects. The reason is that a utility has no natural end. A machine is a bounded object; a compressed air supply is a network that starts somewhere in the building and has to arrive at a specific fitting at a specific pressure. Somewhere along that path the responsibility changes hands, and if that point is not written down, both sides will describe the same installation as complete. The published layout requirements for the equipment are the sensible starting reference, because they define what has to be present at the machine: compressed air above 7 kg/cm², single-phase 220 V and three-phase 380 V both within plus or minus 10 percent, exhaust at 500 cubic feet per minute or about 14.15 cubic meters per minute per connection, working illumination of 800 to 1200 lux with 300 lux as the floor, and an ambient of 23 degrees plus or minus 3 with 45 to 70 percent relative humidity. Those are the conditions the machines need. They are not the scope, because they say nothing about who provides them.
Write each utility as a handover point with a location, a value and a date. Compressed air: the buyer provides a dry, oil-free supply at above 7 kg/cm² to a fitting within a stated distance of each machine inlet, tested and proven before the installation window opens. Electrical: the buyer provides an energised distribution board with the specified single-phase and three-phase feeds, terminated at a labelled isolator for each machine. Exhaust: the buyer provides a duct connection at a stated flange height and size, with the specified flow available at that flange and not merely at the fan. Lighting and environment: the buyer provides the stated illumination at the working plane and the stated temperature and humidity band under normal operation. Network: the buyer provides a live data outlet at each station that requires one. Each of those sentences can be verified by a third party with a gauge, a meter and a date, which is exactly the property missing from the phrase "utilities by buyer". If the project has multiple machines sharing a service, add the sum rather than the single value, because three machines each needing 500 cubic feet per minute require a header sized for 1,500, and headers are routinely designed from the nameplate of one unit.
Utility | Value required at the handover point | Where it is measured |
|---|---|---|
Compressed air | Above 7 kg/cm², dry and oil-free, continuous during production | At the machine inlet coupling, with a gauge and a flow test |
Electrical | 220 V single-phase and 380 V three-phase, both within plus or minus 10 percent, at 50 or 60 Hz | At the isolator serving each machine, under load |
Exhaust | At least 500 CFM, about 14.15 m³/min, per connection | At the duct flange at the machine, not at the fan outlet |
Lighting and environment | 800 to 1200 lux at the working plane, 300 lux minimum; 23 ± 3 °C; 45 to 70 percent RH | At the working plane and at operator height, during a normal shift |
Network | A live data outlet at each station that reports to a system | At the outlet, with a test device, before commissioning |
The duct is the clearest example of a scope that splits badly. A machine supplier will normally provide the extraction hood and the short stub at the machine; a local contractor will normally build the run to atmosphere. The gap between those two is the last metre, and it is where the argument happens. Three arrangements work. In the first, the buyer contracts the whole duct from stub to stack and the supplier only guarantees the flow at the stub. In the second, the supplier takes the whole duct as a design-and-build item, which is cleaner contractually but usually more expensive and slower because it depends on a subcontractor the supplier does not control. In the third, the buyer builds the run and the supplier supplies a commissioning measurement at the flange, which is the cheapest option and requires the buyer to accept flow risk. Whichever is chosen, write the flange size, height and position into the scope, and require the flow to be measured there rather than at the fan outlet, because a long horizontal run with elbows can lose a large share of the nominal capacity before the air ever reaches the hood.
Civil scope is usually discussed as "the building is ready", which is a statement about walls rather than about the three things that actually stop an installation. Floor loading is the first: a machine's static weight is one number, and the point load under a levelling foot during positioning is another, often several times larger. If the floor is a suspended slab or an upper storey, the check has to happen before the machine is ordered rather than when the riggers arrive. Access is the second: door widths, corridor turns, lift capacity and the height of the lowest obstruction all determine whether a machine can reach its position, and a crate that cannot enter the building has to be unpacked outside in weather. Rigging is the third: who supplies the crane, the forklift, the skating equipment and the riggers, and who carries insurance during the lift. These three items are cheap to write and expensive to discover. A single line per machine — weight, footprint, access route, lifting method, responsible party — closes the whole category.
Statutory items are the ones a foreign supplier cannot hold, and buyers routinely assume they are included because they were never mentioned. Which permits are needed depends on the jurisdiction and on what the plant stores and emits: a coating bay with solvent-based material usually triggers flammable storage rules, fire-rated construction and possibly an environmental permit for volatile emissions; a washing step can trigger a wastewater discharge consent; a solder process can trigger fume emission requirements. None of those are equipment scope, and none of them can be delegated to a supplier who is not the local legal entity. Write them as buyer obligations with a named responsible person and a target date ahead of commissioning, because a plant that is mechanically complete but legally unable to store its own coating material is not a plant that can run. The same paragraph should name the inspection authority and the document the authority will ask for, since that document is often a certificate the supplier has to provide and rarely knows is needed.
These three blocks share a property that makes them easy to under-specify: they are not objects, so they cannot be counted on a delivery note. Training is delivered as hours that may or may not have produced competence. Spares are delivered as a list that may or may not be on the shelf. Documentation is delivered as a folder that may or may not be usable by the person who has to maintain the machine in two years. Because none of them can be checked by counting, each has to be specified by an acceptance criterion instead. The pattern is the same in all three cases: name the deliverable, name who receives it, name how it will be judged, and name what happens if it falls short. A project that does this for training, spares and documentation will find that the rest of the scope is easier to enforce, because these three set the tone that the contract is about outcomes rather than shipments.
Training scope needs four numbers and one document. The numbers are: how many people, in which roles, for how many hours, at which location. The document is the competency record. Roles matter more than headcount, because an operator, a programmer and a maintenance technician need different content, and a single combined session for all three produces three people who each learned a third of what they needed. Location matters because factory training on a machine that is already commissioned in the supplier's hall is materially better than classroom training, and on-site training during commissioning is better still for the maintenance technician who has to open the panels. Write the acceptance criterion as a practical test rather than attendance: an operator who can perform a feeder change, a product changeover and a first-article check unaided; a technician who can replace a nozzle, clean a camera and interpret an alarm log. Attendance sheets prove nothing; a signed-off practical test does. Record who signed it, and file the record with the machine documentation rather than with the training file, because the maintenance technician who needs it in two years will look for it next to the machine.
The difference between a recommended spares list and a committed stock is the difference between advice and inventory, and the price difference is substantial. A recommendation lists parts worth holding; a commitment says which of them will be on the buyer's shelf on the day of handover, in what quantity, at what price, and with what replenishment lead time thereafter. Specify the commitment tier by consequence rather than by cost: parts whose failure stops the line and whose lead time exceeds the acceptable stop duration must be held; parts whose failure degrades output can be held at lower quantity; parts available locally within a day need not be held at all. Two clauses make the commitment real. The first is a lead-time table for consumables and wear parts, since a spare that arrives in eight weeks is not a spare. The second is a price-hold period for replenishment, because a first stock priced attractively and a second order priced at list is a common and expensive surprise.
Documentation is the deliverable with the longest life and the shortest specification. Four attributes have to be written down. Format: whether drawings are PDF only or include editable files, because a maintenance team that cannot edit a schematic will redraw it by hand. Language: the language of the operating manual and, separately, the language of the safety labels on the machine, which is a compliance matter in many jurisdictions and cannot be changed after shipment without replacing physical labels. Revision control: how updates are issued after handover, and whether the buyer receives them for the life of the machine or only during warranty. Completeness: the specific list — electrical schematics, pneumatic diagrams, spare parts catalogue with part numbers, PLC and motion programs with a backup method, calibration certificates, material certificates for contact parts, and the acceptance test records from commissioning. The last item is the one buyers regret not asking for, because it is the only objective record of how the line performed on the day it was accepted.

An exclusions list reads like a defensive document and functions as a cooperative one. Its real purpose is not to protect the supplier from claims; it is to force the buyer to look at every item that is not being bought, and to decide deliberately whether the gap is acceptable. A turnkey PCBA factory scope of supply checklist without exclusions is incomplete in a way that is invisible until installation, because every unlisted item defaults to whoever is on site when the question is asked, and that is rarely the party best placed to do the work. Nine exclusions cover most of the exposure in a typical project, and writing them takes less than an hour. The discipline is to write them positively — "buyer supplies and installs" rather than "excluded" — because a positive statement names an owner, while the word "excluded" only names an absence.
The nine, in the order they usually surface: civil and building works, including floor preparation, pits, partitions and doors; utility supply beyond the defined handover points; ductwork beyond the machine stub; statutory permits, inspections and certificates; lifting and rigging equipment and personnel; unpacking, positioning and assembly labour on site where the supplier's scope stops at delivery; consumables used during commissioning beyond a stated allowance, such as paste, stencil, solder, flux and coating material; production materials and the buyer's product for trials; and local taxes, duties and inland transport beyond the agreed Incoterms point. Two of these deserve special attention because they are frequently misread as included. Commissioning consumables are a real cost in a plant that has never run, since the first trials consume paste and solder before any saleable product exists. And duties and inland transport are the items where a delivered price is quoted and an ex-works price is what the contract actually says, which is discovered at the port.
Take an illustrative case, with every figure an assumption. A project writes three exclusions imprecisely: the duct run is described as "site", the first spares stock is described as "recommended", and the second-shift training is not mentioned at all. During installation the duct is found to need 22 metres of galvanised run with two bends, quoted by a local contractor at the equivalent of 8,000 in the buyer's currency, on a three-week lead time. The spares enquiry returns 15,000 for the list the supplier recommended, arriving eight weeks after handover. The second shift is trained by the first shift, informally, and a feeder setup error in month two costs a day of rework. None of those numbers is a claim about any real project; they are the shape of the arithmetic. The point is that the total is not the sum of three line items — it is the sum plus the schedule effect of discovering them after the installation window has opened, when every change is a variation and every variation has a premium.
Each of the twelve blocks needs one acceptance criterion that is objective enough to close it. For process equipment the criterion is a production trial at an agreed rate with an agreed first-pass yield, on the buyer's product, witnessed and recorded. For utilities the criterion is a measurement at the handover point, taken with the buyer's instrument and recorded on a form. For inspection blocks the criterion is detection of a seeded defect set, not the presence of a machine. For MES the criterion is a data point visible in the consuming system. For training it is a practical test signed by the trainer and the trainee's supervisor. For spares it is a physical count against the committed list on the handover date. For documentation it is a document list checked item by item, with the language and format verified. A block without a criterion is a block that cannot be signed off, and a project with several such blocks tends to end in a general acceptance that nobody can date.
The matrix is the working document that sits between the block list and the RFQ. It is one row per deliverable, not one row per block, which typically produces sixty to a hundred rows for a mid-size plant. The columns are the ones described earlier — item, in scope, out of scope, interface, acceptance criterion, target date — plus a column for the question to be asked in the RFQ where the answer is not yet known. The row count itself is a useful signal: a project that starts with a flexible semi-automatic SMD line for an unsettled mix carries far fewer rows than a fully automated plant, and a matrix that is oversized for the phase being bought is a sign that the scope has absorbed equipment the project has not yet justified. Building the matrix takes two days for a project of that size and it replaces the several rounds of clarification that otherwise follow the first quotation. A turnkey PCBA factory scope of supply checklist built this way also has a useful property after the contract is signed: it becomes the acceptance schedule, so the same document that defined the purchase defines the handover, and the two cannot drift apart.
Item (extract) | In scope | Out of scope | Interface |
|---|---|---|---|
SMT line | Printer, mounter, reflow, loader, unloader, inline AOI | Feeder expansion beyond quoted count | Conveyor height 900 mm, SMEMA-compatible handshake at both ends |
Compressed air | Machine-side regulator and filter | Compressor, dryer, main run | Dry air above 7 kg/cm² at a 12 mm quick coupling within 2 m of the inlet |
Exhaust | Hood and stub at the machine | Duct run to atmosphere, stack, fan | Flange diameter and height as drawn, flow measured at the flange |
Power | Control cabinet and flying lead with plug | Distribution board, cable tray, isolator | 32 A three-phase socket within 5 m, energised before installation |
MES data | Data points and protocol documentation per machine | MES software, servers, licences | Points readable by the buyer's gateway within 30 days of handover |
Training | Operator, programmer and maintenance sessions at the factory | Second-shift training, refresher courses | Named attendees, practical test signed off per role |
Spares | Committed first stock per agreed list | Consumables and wear parts beyond the list | Physical count at handover, lead-time table attached |
Documentation | Manuals, schematics, part catalogue, program backups | Translation beyond the agreed language | Editable files for schematics, revision service during warranty |
Start from the block list and expand each block into deliverables, using the acceptance criterion as the prompt: if you cannot state how the item will be accepted, it is not yet a deliverable and probably needs splitting. A row that reads "SMT line — accept at rated output" is too coarse to accept; it becomes printer installation, mounter installation, reflow installation, conveyor handshake, first-article approval and a production trial, each with its own criterion. The reverse error is also common: rows so fine that the matrix becomes a shipping list and nobody can see the structure. A workable size is a row per object that a person could point at. Where the buyer does not know the answer, the row should carry an open question rather than a guess, and the open questions become the numbered queries attached to the RFQ, which is a far better use of the first supplier meeting than a general discussion. Assume nothing about the answer and record who answered it and when.
A simple scoring pass catches the gaps that reading does not. Give every row three points: one for a stated in-scope object, one for a stated interface, one for a stated acceptance criterion. A row that scores three is closed; a row that scores two needs a query; a row that scores one is a heading pretending to be a deliverable. Then score the matrix as a whole on four counts: the proportion of rows at three points, the number of open questions, the number of rows whose owner is "shared", and the number of rows with no date. A matrix with more than about one in five rows at two points, or more than a handful of shared owners, is not ready to be an RFQ attachment, because every one of those gaps will be resolved by the supplier's assumption rather than the buyer's intention. The scoring takes an hour and it is the cheapest review in the project.
Put ten working days between the finished matrix and the RFQ issue, and use them for three passes. First, an internal pass with production, maintenance and finance in the same room, because each of them owns rows the others will not notice: maintenance owns the spares and documentation rows, production owns the training and material handling rows, finance owns the payment, duty and freight rows. Second, a dimensional pass with the building: walk the route from the loading door to the machine position with a tape, and confirm every interface dimension in the matrix against the actual floor, ceiling and door. Third, a supplier pass with one preferred supplier, under a confidentiality understanding, asking only one question: which rows are unclear. That pass is worth more than any amount of internal review, because a supplier reading a scope for the first time sees exactly where the assumptions are, and their answers tell you which rows you have not finished. Ten days spent this way typically removes most of the clarification round that otherwise follows the first quotation.
The scope and the RFQ are different documents with different jobs, and confusing them is why so many RFQs are answered with a price and no structure. The scope says what the boundary is; the RFQ says what you want done about it, in what order, by when, and on what commercial terms. Once the scope is finished, the RFQ becomes short, because most of the technical content is already attached rather than written into the asking document. Five sections carry over from the scope with only their framing changed, and everything else in the RFQ is commercial. Factories that make this separation report a different quality of answer: instead of a single lump price, they receive a price broken down by block, with deviations stated against the matrix, which is the only form in which two quotations can actually be compared.
The five are: the block list, which becomes the pricing structure; the interface schedule, which becomes the responsibility matrix; the exclusions, which become the assumptions each bidder must confirm rather than silently reinterpret; the acceptance criteria, which become the basis for the payment milestones; and the documentation and training lists, which become deliverable items with dates rather than goodwill. The framing change is that each item must now be answered rather than merely stated. A block list in the RFQ should require a price per block and a statement of what is included in it, so that a bidder who has priced a core SMT package and a bidder who has priced a fully automated one are visibly different rather than invisibly cheap and expensive. If the first block is being bought at a semi-automatic level to keep capital low while the mix settles, say so in the RFQ rather than leaving it to be inferred, because a semi-automatic SMT line as the first block in scope will be quoted very differently by suppliers who understand the intent and those who do not.
Attach the matrix as a spreadsheet, not a PDF, so that bidders can add a response column without retyping your rows — a bidder who has to retype will summarise, and summarising is where deviations disappear. Attach the route decision as a one-page narrative, since the blocks only make sense against it. Attach the site information that constrains the answer: floor plan with dimensions, available utility capacities measured at the point of connection, ceiling height and access route, and any known restriction such as a floor loading limit or a landlord's rule about external ductwork. And attach the input package that the commercial side of the enquiry depends on, which is the subject of the input package an RFQ is built from — product definition, volume and shift pattern, quality standard, automation intent, budget band and target production date. Two documents, one matrix and one narrative, are enough. A forty-page specification with no matrix produces a forty-page quotation with no boundary.
When the quotations come back, three questions separate a real answer from a price. First: which rows of the matrix are you not covering, and what do you assume the buyer will do instead? A bidder who returns the matrix with every row marked will have marked some wrongly, and the ones marked wrongly are the ones you want to find now. Second: what is your commissioning sequence and how many working days does each block need on site? A quotation with no sequence has not been planned, and a planned sequence is the only way to check that the utility dates in your own scope are compatible with the supplier's arrival. Third: what is excluded from the acceptance criteria — specifically, what would cause the production trial to be repeated at whose cost? That question is uncomfortable to ask and it is the one that establishes whether the acceptance criteria are a shared target or a formality. A supplier who answers all three in writing has read the scope, which is the minimum qualification for the project.
Send the matrix, not the wish list
If a turnkey PCBA factory is on your capital plan, the most useful thing you can prepare this month is the scope matrix, not the specification. Fill in the twelve blocks, expand each one into objects a person could point at, and mark every row with an interface and an acceptance criterion. Where you do not know the answer, write the question instead of guessing — those questions become the numbered queries that make the first supplier meeting productive rather than introductory. Then send the matrix with your route decision, your site constraints and your volume and quality expectations, and ask for a price per block with deviations stated row by row. We will read it the same way: what is inside the boundary, what is outside it, which interfaces you are keeping and which you expect us to close, and whether the acceptance criteria you have written can actually be demonstrated on your product in your building. Where the matrix has gaps we will say so before quoting rather than after, and where a block is better postponed than bought we will say that too, because a scope that overstates the first phase is the most common reason a plant is commissioned and then left half loaded. What we will not do is quote a single number against a wish list and let the boundary be discovered on site, because a turnkey PCBA factory scope of supply checklist that is never tested against a real quotation is just a document, and the point of writing it was to make the quotation testable.
Scope of supply describes the objects delivered: equipment, documentation, spare parts, training sessions. Scope of work describes the activities performed: installation, commissioning, testing, integration, handover. A turnkey project normally includes both, and the two are frequently written as one list, which is how items disappear. A machine can be in the supply scope and outside the work scope — delivered but not installed — and that combination is common and entirely legitimate, provided it is written down. Write them as two columns against the same rows rather than as two separate documents, because the failure mode is a row that appears in neither.
Detailed enough that every row has an object, an interface and an acceptance criterion, and no more. The test is whether two people who have not spoken could agree on who buys a given cable. Beyond that point, additional detail tends to constrain the supplier's engineering without improving the boundary, and it also lengthens the document until nobody reads it. A mid-size plant typically reaches sixty to a hundred rows. If the matrix runs to several hundred, it has probably become a shipping list; if it runs to twenty, it is still a wish list with headings.
The buyer, almost always, with the equipment supplier responsible for exposing data in a documented form. The reason is that MES is a factory-wide system serving functions the equipment supplier does not control, and no equipment vendor can accept responsibility for a system that spans machines from several suppliers. Split the block explicitly: the supplier delivers data points, protocol documentation and a working test point per machine; the buyer owns the gateway, the system of record and the acceptance test in the consuming system. Write the test as a data point observed in the buyer's system within a stated number of days of handover, because "MES-ready" is not a testable condition.
Sometimes, but rarely as standard, and almost never across borders. Civil work depends on local contractors, local codes and local inspection, and an equipment supplier is usually not the right legal entity to carry it. When it is included, it is normally subcontracted with the supplier taking coordination risk rather than construction risk, and the price reflects that. The practical approach is to keep civil works on the buyer's side and to define the handover point precisely: a floor at a stated level and loading capacity, doors and access route confirmed by measurement, and utility connections at stated positions. That gives the supplier a fixed starting condition and gives the buyer control of the work that is hardest to schedule remotely.
Parts whose failure stops the line and whose replenishment lead time exceeds the stop duration the plant can tolerate. That is a consequence test rather than a cost test, and it usually produces a shorter list than a supplier's standard recommendation, focused on nozzles, feeders, sensors, belts, heaters and control components rather than on complete assemblies. Two things make the commitment usable: a lead-time table covering every listed item, and a price-hold period for replenishment so that the second order is not priced at list. Ask also which items the supplier holds in a local warehouse, since a part held regionally behaves like a shorter lead time without appearing on the stock list at all.
Specify it as three separate deliverables rather than one. First, factory training during commissioning for named roles, in the working language of the plant, with a practical test per role. Second, a train-the-trainer session for two or three people who will deliver the second-shift and future training, which is cheaper than bringing the supplier back. Third, a written record — the manual in the plant language plus the signed practical tests — so that a new operator in two years is trained against a document rather than against someone's memory. Where the machine's safety labels must be in a specific language for compliance, that has to be agreed before shipment, because it cannot be corrected on site.
Leaving the interface to be resolved by goodwill. Almost every scope that goes wrong has the same shape: the blocks are described with reasonable care, the equipment is specified in detail, and the last metre between two scopes is not described at all. It is not a knowledge problem — buyers usually know the duct has to reach the machine — it is a writing problem, because the interface sits between two categories and each category feels complete without it. The remedy is mechanical: require every row to name an interface point with a dimension or a value, and refuse to close a row that has none. That single rule catches most of the exposure, and it costs nothing to apply, which is why a turnkey PCBA factory scope of supply checklist is best built by the person who will have to live with the installation rather than by the person negotiating the price.