English
Views: 0 Author: Site Editor Publish Time: 2026-09-24 Origin: Site


Surface Mount Technology (SMT) manufacturing faces a constant operational tension. You must balance shrinking batch sizes against the demand for maximum throughput. Misaligning your automated robotic systems with actual production profiles introduces severe operational risks. Optimizing for raw speed when your facility requires frequent changeovers leads to idle time. Conversely, over-indexing on flexibility in a high-volume environment creates massive production bottlenecks. You need the right equipment to maintain efficiency and keep your lines running.
This evaluation compares the Hanwha vs Europlacer SMT Pick and Place Machine architectures. While the broader market includes players like ASMPT and Universal Instruments, we focus specifically on Hanwha and Europlacer. We analyze architectural differences, feeder capacities, changeover agility, and long-term scalability. This analysis helps you determine the correct fit for specific Electronic Manufacturing Services (EMS) and OEM environments. Choosing the right platform ensures your production lines run smoothly and adapt to your specific product mix.
Production Alignment: Hanwha excels in providing scalable solutions for extensive production needs requiring rapid throughput, while Europlacer dominates in high-mix scenarios demanding maximum flexibility across diverse production requirements.
Changeover Economics: Europlacer’s architecture prioritizes massive on-machine feeder capacities to minimize teardown and setup times for complex, varied Bill of Materials (BOMs).
Scalability & Modularity: Hanwha provides highly modular platforms that allow manufacturers to scale placement heads and gantries linearly as production volumes increase.
Table of Contents
Choosing an SMT pick and place machine requires more than comparing maximum CPH. Actual production efficiency also depends on changeover frequency, component mix, feeder capacity, and PCB requirements.
CPH: Shows theoretical placement speed, but actual output is usually lower.
Feeder Capacity: Determines how many component types can stay loaded.
Component Range: Check support for 01005 parts, ICs, and odd-form components.
Placement Accuracy: Affects solder quality and downstream rework.
PCB Size: Determines which board and panel sizes the machine can handle.
NPI Frequency: Frequent new products increase the importance of fast changeovers.
Production Type | Main Priority | Machine Requirement |
|---|---|---|
High-Volume | Maximum output | High CPH and continuous operation |
High-Mix | Fast changeovers | High feeder capacity and flexible setup |
Frequent NPI | Less setup time | Offline programming and quick feeder changes |
Stable Production | Consistent speed | High-speed placement and line scalability |
In general, Hanwha focuses on modular, high-speed production, while Europlacer focuses on flexibility, complex BOMs, and frequent product changes. The right choice depends on your actual production mix rather than theoretical machine speed alone.
Hanwha SMT machines focus on high-speed, continuous production. The Decan and SM series use modular gantry systems, multi-nozzle placement heads, and flying vision to maintain fast and accurate component placement.
Dual-Gantry Design: Supports simultaneous picking and placing.
Multi-Nozzle Heads: Improve throughput for standard components.
Flying Vision: Inspects components during movement to reduce delays.
Modular Design: Allows manufacturers to expand capacity as production grows.
Dual-Lane Options: Help reduce PCB transfer time and improve line output.
Hanwha machines are well suited for high-volume EMS, consumer electronics, and automotive PCB production. They perform best when product types remain stable and long production runs require consistent output.
Offline feeder preparation and barcode verification can reduce changeover time and loading errors. Operators should also regularly clean nozzles, check vacuum channels, and replace filters to maintain placement performance.
Hanwha’s modular design can require more floor space as production capacity expands. Frequent changeovers may also reduce the advantage of its high-speed heads, so it is better suited to high-volume and relatively stable production than frequent prototype runs.
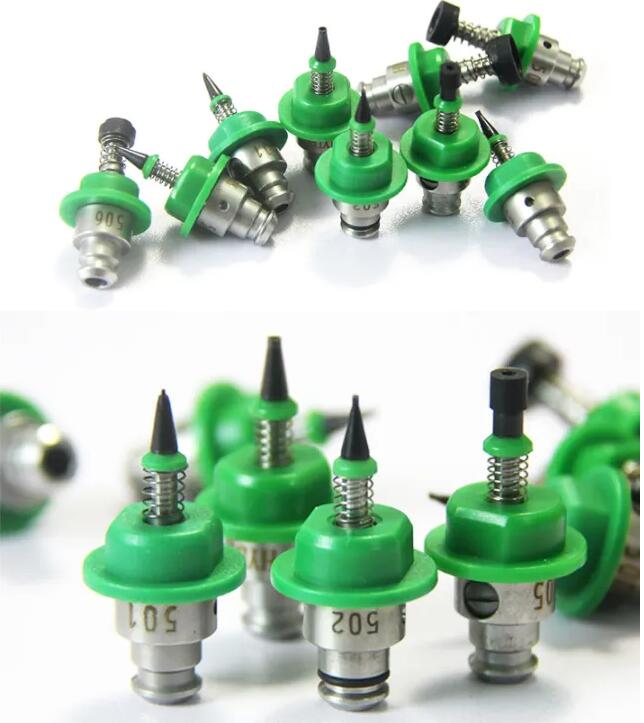
Europlacer SMT machines focus on flexibility, high feeder capacity, and fast changeovers. The iineo+ platform uses a multi-function turret head that handles micro-components, ICs, and large connectors without frequent head changes.
Multi-Function Turret Head: Handles a wide range of component sizes.
High Feeder Capacity: Keeps more components loaded for different jobs.
On-the-Fly Vision: Inspects components during placement.
Automatic Nozzle Selection: Reduces manual head changes.
Flexible Production: Supports different BOMs and frequent product changes.
Europlacer is well suited for high-mix, low-volume production, prototyping, complex EMS projects, aerospace, and other complex PCB assemblies. Its high feeder capacity helps factories move between different products with less setup time.
The machine automatically selects suitable nozzles and inspects components during placement. Operators mainly need to keep nozzle magazines clean and correctly stocked. High feeder capacity also reduces frequent reel changes during production.
Europlacer focuses more on flexibility than maximum raw CPH. For factories producing simple boards in very large volumes, some of this flexibility may not be fully used.
Hanwha and Europlacer use different approaches to improve SMT production. Hanwha focuses on high-speed modular production, while Europlacer focuses on high-mix flexibility and reducing changeover time.
Factor | Hanwha | Europlacer |
|---|---|---|
Main Focus | High-speed production | Flexible production |
Placement Head | Inline multi-nozzle | Multi-function turret |
Feeder System | Modular feeder carts | High on-machine feeder capacity |
Changeovers | Offline cart preparation | More components remain loaded |
Component Range | Standard chips and ICs | Wide range and odd-form parts |
Best Fit | High-volume, stable production | High-mix, frequent NPI |
Expansion | Add modular machines | High capacity in one machine |
Both Pick and Place Machines support MES integration, offline programming, and component traceability. They can exchange production data through protocols such as IPC-CFX and SECS/GEM, helping factories manage production and prepare new jobs while machines remain in operation.
Both platforms require regular calibration, nozzle maintenance, and inspection to maintain placement accuracy. Buyers should also consider power, compressed air, spare parts, and access to internal components because these factors can affect long-term uptime and maintenance costs.
Hanwha is designed around speed, modular expansion, and stable high-volume production. Europlacer places greater emphasis on feeder capacity, complex component handling, and frequent changeovers. The better fit therefore depends on production volume, BOM complexity, NPI frequency, and available floor space.
Evaluation Criteria | Hanwha Architecture | Europlacer Architecture |
|---|---|---|
Primary Focus | Raw throughput and modular scalability | Maximum flexibility and changeover agility |
Placement Head Style | Inline multi-nozzle heads | Multi-function turret heads |
Feeder Strategy | Rapid-swap modular feeder carts | Massive resident on-machine capacity |
Ideal Environment | High-volume, stable product mix | High-mix, frequent NPIs, complex BOMs |
Vision System | High-speed flying vision | Integrated on-the-fly inspection |
Floor Space Efficiency | Requires linear expansion for capacity | High capacity within a single footprint |
Component Handling | Optimized for standard chips and ICs | Optimized for extreme variance and odd-form |
Buying SMT equipment involves more than comparing speed and placement accuracy. Training, local technical support, spare parts, and software integration can all affect long-term production efficiency.
Hanwha and Europlacer use different software, feeder systems, and operating methods. Operators should receive training before installation so they can manage feeders, changeovers, vision errors, and basic troubleshooting.
Local technical support can reduce downtime when equipment problems occur. Before purchasing, check the supplier’s Service Level Agreement (SLA), engineer response time, and local availability of key parts such as nozzles, belts, motors, and filters.
New SMT machines should work smoothly with existing MES and production systems. Test data exchange, traceability, CAD/BOM import, and offline programming before installation to avoid integration problems later.
Check power, compressed air, network, and floor requirements.
Complete operator and maintenance training before installation.
Run a pilot batch to test placement and vision systems.
Test MES connections and PCB traceability.
Prepare common spare parts and consumables.
Calibrate feeder carts or feeder banks before production.
These checks can reduce installation delays and help the new SMT machine reach stable production faster.
The choice between Hanwha and Europlacer is not about which machine is objectively superior. It is about which architecture aligns with your facility's specific NPI rate, volume demands, and regional support infrastructure. You must match the machine's core design philosophy to your daily operational reality. Misalignment leads to idle equipment or massive bottlenecks.
Recommend Hanwha for operations where scaling raw throughput and managing extensive production needs are the primary drivers. If you run large batches of stable products, Hanwha’s modular speed delivers exceptional results. Recommend Europlacer for operations where minimizing changeover downtime and handling complex BOMs dictate success. If you face frequent NPIs and require extreme flexibility from prototyping to volume production, Europlacer provides the necessary agility.
Take the following actionable steps to finalize your decision:
Conduct a comprehensive time-study using your most complex BOMs on both platforms to measure true changeover times.
Request live offline programming software demos using your native CAD files to evaluate the user interface.
Calculate realistic CPH based on your specific product mix rather than relying on theoretical maximums.
Audit the local spare parts inventory and review the Service Level Agreements with regional distributors.
A: Hanwha prioritizes modular scalability and high-speed volume for extensive production using inline heads. Europlacer prioritizes industry-leading feeder counts and multi-function flexibility using turret heads to handle complex, high-mix environments without requiring head changes.
A: Europlacer is widely recognized for this environment. Platforms like the iineo+ utilize multi-function heads and massive continuous feeder capacity. This architecture drastically reduces setup times and allows multiple distinct product runs to be loaded simultaneously.
A: Yes, Hanwha machines are highly suitable for EMS providers handling varied but generally higher volumes. Their modular design allows an EMS to expand lines linearly to meet aggressive throughput goals as client demands increase.
A: Higher on-machine feeder capacity allows multiple product BOMs to be loaded simultaneously. This drastically reduces changeover downtime between runs. Operators spend less time tearing down and setting up carts, leading to higher overall machine utilization.
A: Evaluate the frequency of routine calibrations, nozzle replacement intervals, and the accessibility of internal belts and motors. You must also verify the local availability of spare parts and the response time guaranteed in your regional Service Level Agreement.
A: Yes, Europlacer machines are designed to adapt from prototyping to high-volume production without sacrificing quality. While their primary operational advantage remains in environments requiring agility, they provide consistent, reliable output for sustained production runs.